Expert advice, industry updates, cut & sew guides, and private label fashion trends.
Learn how to build patterns, source fabrics, and turn designs into commercial apparel.
Discover tips on screen printing, embroidery, fabric sourcing, and private label scaling.
Choosing the right printing method can shape your brand’s quality, costs, and customer experience. Direct to Garment Printing offers detailed, full-color designs without traditional screen setup. It can suit small batches, custom orders, and test collections. However, it is not automatically the best choice for every business.
A reliable decision begins with your products. Check whether your garments contain enough cotton for strong ink absorption. Examine fabric weight, seams, stretch, and washing requirements. A soft cotton shirt may produce bright, comfortable results. A dark polyester hoodie may require different equipment or pretreatment. These details matter more than attractive machine specifications.
Your artwork also deserves practical testing. Fine lines, pale colors, and large solid areas can behave differently on fabric. Request physical samples before approving a supplier or purchasing equipment. Hold the shirt under natural light. Wash it several times. Inspect cracking, fading, texture, and color consistency. The first sample may disappoint. That is useful evidence, not wasted effort.
Business planning is equally important. Compare printer costs, pretreatment tools, curing equipment, labor, maintenance, ink usage, and production speed. A low entry price can hide expensive daily requirements. Direct to Garment Printing may reduce inventory risk, but slow production can affect larger orders. Consider customer demand honestly.
No method is perfect. A careful choice balances print quality, order volume, garment range, workflow, and long-term reliability. Consult experienced suppliers, review technical documentation, and confirm safety requirements for inks and workplace operations. Your final decision should come from tested results, not promises alone.
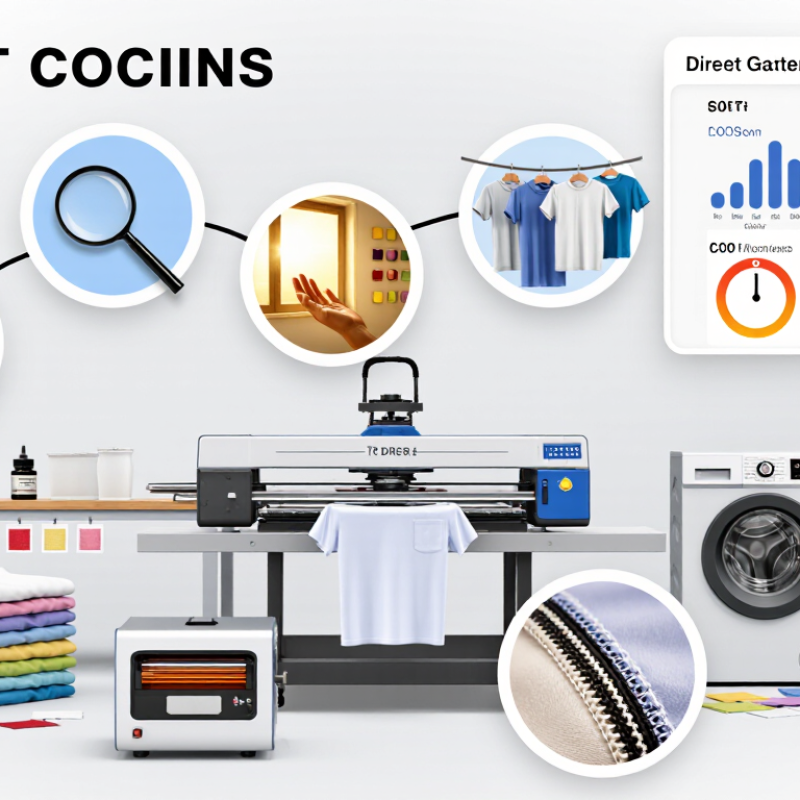
Direct-to-garment printing places water-based ink directly onto a finished garment. The core process starts with artwork preparation and fabric inspection. Operators then load the garment onto a flat platen. The surface is pretreated, usually to help white ink bond with dark fabrics. After printing, heat curing fixes the ink inside the fibers.
The workflow is compact, but each stage affects the final result. A slightly uneven collar can create blurred edges. Excess pretreatment may leave a stiff patch. White ink also needs careful circulation and calibration. The design usually prints with white ink first, followed by colored layers. Curing temperature and time depend on the garment fabric and ink system. Do not guess here.
Grand View Research reported that the global digital textile printing market was valued at approximately USD 5.4 billion in 2023. Smithers has also identified continued growth in digital textile production, supported by shorter runs and personalized orders. These figures describe digital textile printing broadly, not only direct-to-garment equipment. That distinction matters. In practical production, direct-to-garment printing suits detailed artwork, small batches, and frequent design changes. It may perform less efficiently on very large orders. Cotton often provides strong results, while blends can require testing. Experienced operators should wash-test samples before approving bulk production. Even then, color matching is not perfectly predictable.
Direct-to-garment printing applies water-based ink directly to a prepared garment. The workflow typically includes artwork preparation, pretreatment, drying, printing, and heat curing. The chart shows representative processing times per garment; actual results vary according to fabric type, image size, pretreatment method, printer settings, and curing equipment.
How to Choose Direct to Garment Printing for Your Business
Product choice should begin with the fabric, not the artwork. Direct to garment printing performs best on cotton and cotton-rich shirts. Their absorbent fibers hold water-based ink with strong detail and softer hand feel. Polyester can work, but dye migration may dull light colors. Dark garments also require pretreatment and white ink, which can change texture and cost.
Test the fabric first. Wash it five times. Check cracking, fading, and color shift under daylight. Textile Exchange’s Materials Market Report 2024 states that global fiber production reached 124 million tonnes in 2023. It may reach 160 million tonnes by 2030. That growth makes recycled and blended fabrics more common, but sustainability claims still need supplier verification.
Design requirements should match the garment’s limits. DTG suits photographs, gradients, small orders, and personalized artwork. Use clean transparent files and roughly 300 DPI at final size. Tiny text may lose clarity on textured fabric. Grand View Research forecasts a 19.1% annual growth rate for digital textile printing from 2024 to 2030. Demand is rising, yet speed should not replace testing. A real production sample may expose an expensive mistake. Dark fabric, heavy ink coverage, and oversized graphics can feel less comfortable than expected.
| Product Type | Recommended Fabric | Fabric Suitability | Best Design Characteristics | Pretreatment Requirement | Expected Print Result | Main Production Consideration | Business Use Case |
|---|---|---|---|---|---|---|---|
| Light-Colored T-Shirt | 100% cotton or cotton-rich fabric | Excellent; cotton absorbs water-based DTG ink effectively | Full-color artwork, gradients, photographs, and fine details | Usually required, with a lighter application than for dark garments | Soft hand feel and strong color reproduction on the garment surface | Fabric moisture, pretreatment consistency, and heat curing affect durability | Custom apparel, short-run collections, artwork-led products |
| Dark-Colored T-Shirt | High-cotton fabric, preferably tightly knitted | Very good when white ink is available and properly applied | High-contrast graphics, vivid colors, logos, and photographic images | Required; white ink normally forms an underbase beneath colored ink | Bright, opaque artwork with a slightly heavier ink layer than on light garments | White-ink circulation, underbase density, and curing temperature require control | Streetwear, promotional apparel, team merchandise, and premium graphics |
| Hoodie or Sweatshirt | Cotton or cotton-polyester fleece with a smooth print area | Good; smoother outer surfaces produce sharper edges | Medium-to-large graphics, bold typography, and layered illustrations | Required; absorbency varies with fleece construction and fiber blend | Good coverage, although textured or raised fleece can slightly reduce detail | Garment thickness, seams, pockets, and platen clearance can limit placement | Seasonal collections, fashion merchandise, and higher-value custom products |
| Tank Top or Lightweight Top | Lightweight cotton or cotton-modal fabric | Good when the fabric is stable and not excessively thin | Small-to-medium graphics, line art, text, and lifestyle illustrations | Required; use controlled application to avoid excess stiffness | Soft results are possible, but thin fabrics may show minor ink visibility from the reverse side | Stretch, fabric distortion, and heat sensitivity should be tested before production | Fitness, summer apparel, event merchandise, and small creative collections |
| Canvas Tote Bag | Cotton canvas or other tightly woven natural-fiber canvas | Good if the surface is flat, clean, and not heavily textured | Bold illustrations, simple logos, typography, and limited-color designs | Generally required for consistent ink adhesion and color development | Defined prints with a natural textile appearance | Uneven weave, seams, handles, and bag construction may restrict the printable area | Retail packaging, event giveaways, eco-focused merchandise, and art products |
| Polyester Sportswear | Polyester or performance blends designed for garment printing | Limited with standard DTG inks; specialized processes may be necessary | Simple, high-contrast graphics and designs validated through sample testing | Process-dependent; polyester may require migration control and compatible chemistry | Results vary with fabric dye, ink system, pretreatment, and curing conditions | Dye migration, adhesion, stretch, and repeated washing must be tested carefully | Sports uniforms, activewear, and performance garments after production validation |
| Blended-Fabric Garment | Cotton-polyester blends with a high cotton percentage | Moderate to good; color intensity usually decreases as synthetic content increases | Moderate-detail artwork, solid colors, and designs where a vintage effect is acceptable | Required; use a process suited to the blend and desired color density | Natural, slightly muted colors may occur on fabrics with substantial polyester content | Fiber ratio, fabric color, and dye stability should be confirmed with a physical sample | Cost-conscious apparel lines and products requiring improved shape retention |
| Small Custom Batch | Primarily cotton T-shirts, sweatshirts, or tote bags | Excellent for testing demand and producing varied designs | Variable artwork, personalization, photographs, and one-off designs | Depends on garment color and fabric; each substrate should be profiled | Flexible, detailed output without screen setup for every design | Artwork preparation, garment loading, and pretreatment time influence unit cost | Print-on-demand, prototypes, personalized orders, and market testing |
Choosing direct-to-garment printing starts with production reality, not machine excitement. Grand View Research estimates the global direct-to-garment printing market will grow at an annual rate of about 11.5% from 2024 to 2030. That growth attracts new suppliers, but equipment must match daily order patterns. A compact printer suits short runs and custom artwork. A production unit performs better when orders arrive continuously. Measure garments per hour, setup time, curing time, and operator workload.
Ink systems create different operational demands. Water-based pigment ink usually supports soft hand-feel and detailed graphics on cotton. White ink enables dark garments, but it needs regular circulation and careful maintenance. Neglected white ink can create blocked nozzles, wasted shirts, and unexpected downtime. Pretreatment also matters. Uneven spray can produce dull colors or stiff patches. In my experience, sample testing under actual humidity conditions reveals more than a showroom demonstration.
Production capability includes workflow, not only print speed. Smithers’ The Future of Digital Textile Printing to 2027 reports continued double-digit growth in digitally printed textile output, increasing pressure for dependable automation. Check file preparation, garment loading, curing, inspection, and rework capacity. A printer rated for 40 garments per hour may produce far less during frequent color changes. That gap deserves attention. Ask for verified output using your garments, artwork, and ink settings. Then compare ink consumption, maintenance hours, rejected pieces, and labor costs over a full month. The fastest machine may still be the wrong investment.
Direct-to-garment printing suits businesses selling short runs, personalized apparel, and frequent artwork changes. It removes screens and reduces setup time, but equipment costs can be substantial. Grand View Research valued the global digital textile printing market at approximately US$2.7 billion in 2023. The report also projects strong growth through 2030. Market growth does not guarantee profit. Your order volume matters more.
Calculate cost per wearable item, including ink, pretreatment, labor, rejected garments, and electricity. A practical shop-floor test should compare a ten-shirt order with a hundred-shirt order. Record loading time, curing time, cleaning time, and reprints. Workflow gaps often appear beside the printer, not inside it. A poorly placed pretreatment station can slow production and create uneven results. Small details matter.
Maintenance must be treated as scheduled production work. Daily nozzle checks, regular cleaning, and controlled humidity can protect print quality. Skipping one routine may create costly downtime later. Smithers’ industry analysis identifies digital textile printing as a continuing growth area, supported by customization and shorter production runs. Scalability still requires discipline. Add capacity only after tracking weekly demand, operator hours, and machine utilization. A second printer may increase output, but it can also double maintenance and training needs. I would not rely on optimistic sales forecasts alone. Test real orders, measure actual margins, and accept that some assumptions will fail.
Selecting a direct-to-garment solution starts with your order pattern, not the machine’s advertised speed. Measure weekly volume, artwork complexity, garment colors, and average order value. Grand View Research valued the global digital textile printing market at USD 2.7 billion in 2022 and projected a 12.1% CAGR through 2030. That growth suggests opportunity, but it does not guarantee profit for every workshop.
Request sample prints on your actual shirts. Check fine text, dark fabric coverage, wash durability, color consistency, and curing time. Ask about white-ink circulation, printhead maintenance, software training, and replacement costs. A reliable supplier should provide operating procedures and realistic production tests.
My first cost estimate was too optimistic because cleaning time and rejected garments were missing. That mistake matters. Calculate ink, pretreatment, labor, electricity, maintenance, packaging, and reprints per item. Smithers’ digital textile printing forecasts also highlight continuing investment in shorter runs and on-demand production.
Tips:
Compare three complete workflows, not three machines. Record print time from loading to curing. Wash-test samples after five and twenty cycles. Inspect edges under bright light. Keep one sample from every production batch. Do not trust speed claims without downtime data. A slower system may suit custom orders better. However, a faster system can disappoint when artwork needs frequent color changes. Leave room for training, repairs, and human error. Those costs are easy to underestimate.
Cotton and cotton-rich shirts usually absorb water-based ink well. They support sharp details and a softer feel. Test every fabric.
Yes, but dye migration may dull light colors. Test a sample after curing and washing. Results can vary more than expected.
Wash the printed sample five times. Inspect cracking, fading, and color changes in daylight. A quick test can prevent costly mistakes.
They require pretreatment and white ink. These steps may increase cost and create a heavier texture. Comfort should be checked by hand.
Use clean transparent files at roughly 300 DPI at final size. Photographs, gradients, and personalized artwork often work well. Tiny text may blur.
Uneven pretreatment can create dull colors or stiff patches. Humidity may also change the result. Test under real working conditions.
Compact equipment suits short runs and custom orders. Production equipment fits steady daily demand. Rated speed can mislead.
Track garments per hour, setup time, curing time, ink use, maintenance, labor, and rejected pieces. Measure them for a full month.
White ink needs regular circulation and careful maintenance. Neglect can block nozzles, waste shirts, and cause downtime. This part is easy to underestimate.
No. Frequent color changes, loading delays, and rework can reduce actual output. Use your garments, artwork, and settings for verification. I would question showroom numbers.
Choosing Direct to Garment Printing for your business begins with understanding how the process works and how it applies ink directly onto fabric to create detailed, full-color designs. Before investing, consider the products you plan to offer, including garment types, fabric composition, colors, sizes, and the level of image detail required. These factors will influence print quality, durability, and the suitability of different equipment and ink systems.
A practical decision should also compare production speed, print capacity, operating costs, workspace requirements, and ease of use. Maintenance needs, workflow efficiency, staff training, and ongoing supply expenses can significantly affect profitability. Businesses should evaluate whether the solution supports current demand while allowing room for future growth. By balancing product requirements, equipment performance, total ownership costs, and scalability, you can select a Direct to Garment Printing solution that fits your operational goals and provides consistent value over time.