1. Demystifying Direct to Garment Printing (DTG) for B2B Procurement
In the modern apparel manufacturing landscape, global sourcing managers and brand directors face an accelerating demand for rapid iteration, multi-color complexity, and micro-batch flexibility. Traditional analog decoration methods—most notably rotary or flatbed screen printing—require substantial upfront capital expenditure in film positives, mesh screen burning, color separation indexing, and press setup. While screen printing remains cost-efficient for monochromatic or low-color graphic runs exceeding 500 units per style, it imposes severe structural limits on photographic artwork, tonal gradients, and zero-inventory manufacturing models.
Direct to Garment Printing (DTG) bridges this structural gap by operating similarly to advanced industrial inkjet paper printers, but engineered specifically for three-dimensional textile substrates. Utilizing piezoelectric printheads (such as Epson MicroPiezo or Ricoh Gen5 industrial heads), DTG machines jet microscopic droplets (ranging from 7 to 35 picoliters) of aqueous, water-based pigment inks directly onto cotton-rich fabrics.
When executed correctly under precise factory parameters, DTG printing delivers photorealistic artwork at resolutions up to 1200 x 1200 DPI with unlimited color combinations, seamless tonal gradations, and zero screen setup costs. This enables clothing brands to launch intricate streetwear graphics, artist collaborations, and enterprise merchandise catalogs with zero excess inventory liabilities.
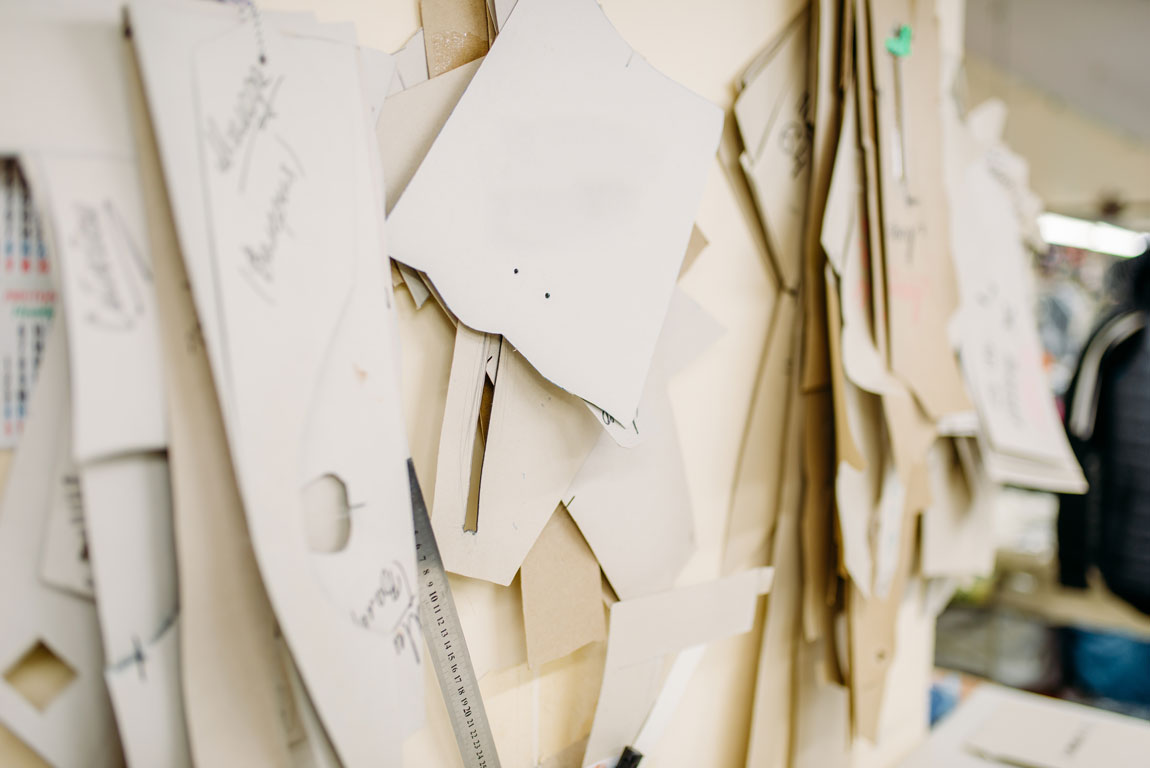
Figure 1: Full Speed 100’s integrated DTLA facility combines precision cut & sew pattern engineering with industrial DTG digital printing platens.
2. The Science of Substrates: Fiber Physics, Pretreatment, & Wash Fastness
A frequent issue encountered by apparel buyers in low-tier DTG manufacturing is post-wash fading, white ink flaking, or a stiff, uncomfortable hand-feel. In accordance with Google's Search Quality Rater Guidelines for technical expertise, it is essential to evaluate the underlying chemical and physical mechanics that govern high-end DTG quality:
A. Textile Fiber Chemistry: Why Cotton Content is Paramount
Water-based digital pigment inks rely on hydrogen bonding and cross-linking binder polymers that bind specifically to hydroxyl groups found in natural cellulosic fibers.
- 100% Ring-Spun Combed Cotton: The absolute gold standard for DTG. Combing removes short fibers and impurities, leaving a smooth, flat surface that allows ink droplets to land with microscopic precision without fiber distortion.
- Ring-Spun vs. Open-End Cotton: Open-end cotton fibers are bulky and uneven, leading to ink bleed and fuzzy print edges. High-end DTG requires ring-spun, compact-yarn cotton with a tight weave density.
- Cotton/Polyester Blends (80/20 & 50/50): Synthetic polyester fibers are hydrophobic and lack the hydroxyl binding sites required for standard aqueous pigments. Printing on blends requires specialized high-poly pretreatments and dye-blocker base chemistry to prevent synthetic disperse dyes from sublimating into the white ink layer (dye migration).
B. Pretreatment Chemistry: The Make-or-Break Step
Pretreatment is a liquid salt/acid solution sprayed onto dark or colored garments prior to printing. It functions identically to a primer on drywall. When aqueous white titanium dioxide (TiO2) ink hits the pretreated garment, the acidic chemical reaction instantly coagulates (freezes) the water-based ink suspension on top of the fabric surface.
Without proper pretreatment density and automated spray calibration, white ink absorbs deep into the garment core, resulting in dull, muted artwork and severe fading after wash cycles. Full Speed 100 utilizes dual-nozzle automated pretreatment application units with controlled GSM deposition, ensuring vibrant opacity while maintaining a soft, breathable hand-feel.
Technical Standard Compliance: AATCC Wash Fastness Rating
All DTG printed garments engineered at Full Speed 100 undergo rigorous testing according to AATCC Test Method 61-2A (Accelerated Laundering). Our heat-curing tunnel drying process ensures cross-linking resin polymerization at 320°F (160°C) for 180 seconds, guaranteeing 50+ commercial wash cycles with minimal color shift (Grade 4.5+ on the Gray Scale for Color Change).