Explore our B2B wholesale activewear line crafted from GRS-certified recycled polymers, bio-based nylon, and OEKO-TEX certified organic blends. Optimized for export compliance and brand customization.
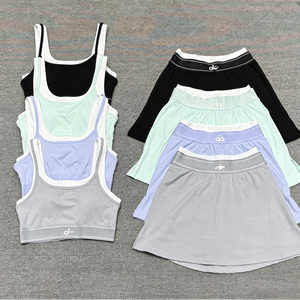
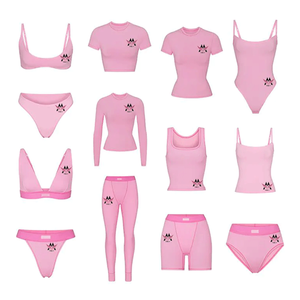
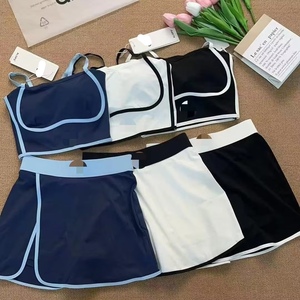
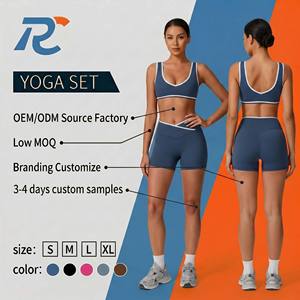
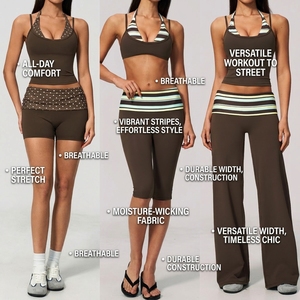
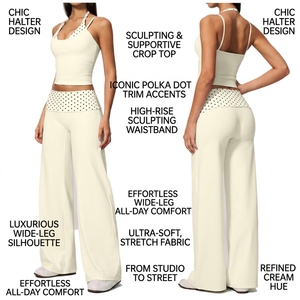
In an era governed by strict European Union environmental mandates and escalating consumer demands for eco-transparency, generic fabric sourcing no longer satisfies global compliance standards. This technical whitepaper establishes the benchmark for CE Certified Sustainable Fabric Sourcing.
Modern apparel brands facing EU Digital Product Passport (DPP) regulations require absolute supply chain verification. As a full-service custom apparel manufacturer headquartered in Los Angeles with global production facilities, Full Speed 100 integrates CE-compliant standards across yarn spinning, eco-friendly dyeing, seamless knitting, and final garment assembly.
Our sustainable fabric sourcing framework eliminates supply chain opacity. By utilizing GRS-certified recycled polyester (rPET), GOTS-certified organic cotton, and closed-loop regenerated cellulose fibers (Tencel™/Modal), we provide enterprise procurement officers with verified Life Cycle Assessment (LCA) data and transaction certificates for every shipment.
| Performance Metric | Standard Synthetic Fabric | CE Certified Recycled Polymer | Bio-Based Circular Textile |
|---|---|---|---|
| Primary Raw Material | Virgin Crude Oil Derivatives | Post-Consumer PET Bottles (GRS) | Bio-Nylon 6,6 / Castor Bean Oil |
| Carbon Footprint (CO2e/kg) | 7.2 kg CO2e | 2.3 kg CO2e (-68%) | 1.8 kg CO2e (-75%) |
| Tensile & Elastic Recovery | Standard Elasticity | Reinforced Mechanical Stretch | High Memory Shape Retaining |
| Chemical Safety & Heavy Metals | Variable / Unchecked | OEKO-TEX Standard 100 Class I | REACH SVHC Candidate Free |
| EU DPP Traceability | Non-Compliant | Fully Traceable TC Blockchain | Digital Twin QR Integrated |
Understanding the technical nuances of CE marking, Personal Protective Equipment (PPE) standards, and chemical safety mandates in international activewear procurement.
Under EU Regulation 2016/425, specialized sports apparel providing compression, UV radiation protection (UPF 50+), or ergonomic joint support must meet fundamental safety and health criteria to carry the CE mark.
All fabric batches undergo rigorous testing for SVHC (Substances of Very High Concern), azo dyes, phthalates, and PFCs (perfluorinated chemicals), guaranteeing 100% compliance with EU REACH chemical restrictions.
Our raw material vendors hold Global Recycled Standard (GRS 4.0) certifications, providing chain-of-custody tracking from recycled plastic scrap to spun yarn and finished elastane activewear sets.
Strategic foresight for apparel brand directors, sourcing agents, and product managers preparing for next-generation circular textile ecosystems.
While standard mechanical recycling degrades polyester fiber length with each iteration, chemical recycling (depolymerization) returns synthetic polymers to virgin-grade monomers. By 2026, premium activewear sourcing will heavily prioritize chemically recycled polyester and elastane, maintaining 100% tensile elasticity across repeated wash cycles.
Traditional elastane (Spandex/Lycra) poses a significant obstacle to circular apparel recycling. Next-gen activewear utilizes bio-derived elastane synthesized from renewable plant starches or degradable TPU compounds, allowing elastane-blended leggings and sports bras to be safely processed in commercial recycling facilities.
Fabric dyeing accounts for up to 20% of global industrial water pollution. FS100 is integrating waterless dye technologies using dry supercritical carbon dioxide (scCO2). This process eliminates liquid wastewater discharge, saves 50% energy, and achieves superior color fastness to washing and light exposure.
Replacing toxic silver ion coatings with plant-based chitosan and botanical peppermint bio-treatments that inhibit odor-causing bacteria for up to 50 home laundries.
Every garment batch is equipped with scannable QR micro-labels linked to immutable blockchain records detailing raw material origin, mill energy sources, and CE test data.
Designing activewear specifically for disassembly, utilizing mono-material yarn construction so that zippers, trims, and main body fabrics can be recycled without sorting.
Headquartered in Los Angeles, California, Full Speed 100 operates a comprehensive design, cut & sew, sourcing, and branding facility delivering high-margin private label apparel solutions worldwide.
Full Speed 100 bridges the gap between boutique fashion brands, high-performance athletic lines, and large-scale enterprise apparel buyers. Our vertically integrated operations support emerging label startups with low Minimum Order Quantities (MOQs) while accommodating scalable bulk container shipments.
Comprehensive 2D/3D digital pattern creation, size grading, marker making, and rapid sample prototyping within 7–10 business days.
Precision computer-controlled fabric cutting, four-needle six-thread flatlock stitching, and rigorous inline quality assurance inspections.
Custom eco-friendly hang tags, recycled woven neck labels, bio-degradable polybags, and custom retail-ready packaging execution.
Analyzing yield optimization, MOQ flexibility, regulatory exposure, and total cost of ownership for commercial apparel procurement.
| Evaluation Factor | Conventional Offshore Sourcing | Full Speed 100 CE Certified Infrastructure | Strategic Brand Benefit |
|---|---|---|---|
| Minimum Order Quantity (MOQ) | 1,000–3,000 Pcs per Color/Style | Low MOQ Flexible Options (100–300 Pcs) | Mitigates Inventory Risk & Working Capital Overhang |
| Fabric Compliance Certification | Self-Declared / Unverified Labs | Third-Party CE, GRS, OEKO-TEX, REACH Verified | Zero Risk of Customs Seizure or Import Fines |
| Sample & Development Lead Time | 4–8 Weeks (Multiple Re-samples) | 7–12 Business Days (High-Precision CAD) | Accelerates Time-to-Market by 65% |
| Fabric Yield & Scrap Waste | 15%–22% Standard Cutting Scrap | Automated CAD Layout Nesting (<8% Scrap) | Substantial Material Cost Savings Passed to Client |
| Branding & Finishing Flexibility | Dispersed Third-Party Vendors | In-House Screen Print, DTG, Embroidery, Heat Transfers | Single Point of Accountability & Flawless Quality |
Expert answers addressing technical specifications, regulatory compliance, custom sampling, MOQ thresholds, and international shipping protocols.
Under EU directives, CE certification for apparel applies when garments provide specific protective or physical performance features (such as UV radiation shielding UPF 50+, high-impact joint support, or anti-static safety properties governed by EU Regulation 2016/425). Our CE-certified fabric mills undergo strict testing for tensile breaking strength, color fastness to perspiration, dimension stability after laundering, and non-toxicity verified under REACH and OEKO-TEX Standard 100.
Every batch of GRS-certified recycled polyester or bio-nylon is backed by official Transaction Certificates (TC) issued by accredited certification bodies (such as Control Union or Intertek). These certificates track the chain of custody from raw post-consumer plastic collection through polymer pelletization, yarn spinning, and final fabric weaving, guaranteeing full audit readiness for your brand.
Unlike restrictive overseas factories requiring thousands of units, Full Speed 100 offers low MOQ custom clothing development programs starting at 100 to 300 pieces per style/colorway depending on fabric customization. For stock wholesale blanks customized with private label branding applications, MOQs can be even lower.
Yes. Our textile dyeing facilities utilize digital Pantone (TPX/TCX) color-matching systems with GOTS and OEKO-TEX certified dyestuffs. We provide lab dips (swatch approvals) within 5–7 business days, ensuring 99.5% color accuracy without utilizing restricted heavy metals or azo dyes.
We provide full-service branding customization under one roof, including ultra-durable silicone heat transfer logos (ideal for high-stretch activewear), breathable direct-to-garment (DTG) printing, high-density screen printing, sublimation for all-over print artwork, and custom 3D puff embroidery. We also handle custom woven labels, heat-seal care tags, and eco-friendly packaging.
Initial prototype samples and tech pack validations typically take 7 to 14 business days. Upon sample approval and fabric lab dip sign-off, full cut & sew bulk manufacturing typically ranges between 3 to 5 weeks depending on order volume and structural complexity. Rush manufacturing options are available upon request.
Absolutly. All sustainable yarns, elastic trims, dyes, and printing inks utilized in our production facilities are tested and confirmed free of toxic phthalates, lead, formaldehyde, and PFAS ("forever chemicals"). Test reports can be provided for compliance verification prior to bulk production.
We supply verified digital data packages for all manufactured garments, detailing raw material composition, supplier origin, certified eco-dyes, life cycle energy metrics, and care longevity instructions. This data can be directly converted into scannable QR micro-labels for seamlessly meeting upcoming EU DPP compliance guidelines.
Engineered for performance, verified for sustainability, and crafted for scale. Contact our Los Angeles product development team today to receive fabric swatches, technical estimates, and custom manufacturing consultation.