Explore our high-demand OEM/ODM product lines engineered with stretch-recovery, moisture management, and tailored athletic fits.
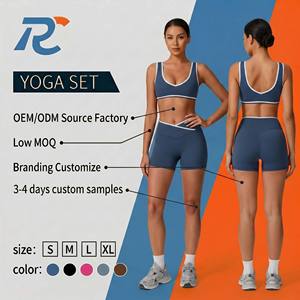
As modern outerwear transitions from purely functional weather protection into highly technical, urban athleisure ("Gorpcore"), procurement executives demand manufacturing partners capable of balancing complex waterproof-breathable laminates with rapid turnaround times, low minimum order quantities (MOQs), and strict quality compliance.
Our dual-studio model combines US-based strategic product development in Los Angeles with high-precision manufacturing centers in China. This hybrid structure gives international buyers the best of both worlds: frictionless design alignment, technical pattern grading, and localized account management coupled with China's unmatched textile supply chain efficiency.
From 3-layer hydrostatic membrane jackets and bonded polar fleece hoodies to high-compression seamless activewear, our technical seam-taping, laser cutting, and ultrasonic welding ensure every garment withstands demanding field conditions while delivering fashion-forward silhouettes.
Global apparel supply chains are shifting rapidly. B2B buyers must navigate evolving sustainability directives, volatile freight dynamics, and shifting consumer behavior.
Regulatory frameworks across North America and Europe are banning per- and polyfluoroalkyl substances (PFAS). Global procurement requires non-fluorinated Durable Water Repellent (C0 DWR) treatments and bio-based TPU membranes that achieve >10,000mm waterproofing without toxic breakdown products.
The boundary between technical outerwear (jackets, parkas, windbreakers) and activewear (seamless leggings, running tops, sports bras) has dissolved. Modern line planning demands hybrid suppliers capable of handling both heavy-gauge woven seam-sealed outerwear and fine-gauge circular knit stretch garments in one unified order.
Over-inventory risk is the #1 margin destroyer for fashion brands. Future-ready procurement relies on 3D CLO digital sampling to eliminate physical sample cycles, paired with flexible order batching (MOQs starting as low as 100-300 pieces per colorway) to enable quick re-orders based on sell-through data.
Comprehensive breakdown of fabric structures, membrane ratings, and seam constructions engineered for high-performance applications.
| Garment Category | Fabric Construction | Hydrostatic Pressure (Waterproof) | Breathability (MVTR) | Recommended Seam Technique |
|---|---|---|---|---|
| Alpine / Expedition Outerwear | 3-Layer (3L) 70D Recycled Nylon Ripstop + ePTFE Membrane | 20,000 mm H2O | 20,000 g/m²/24hr | 100% Fully Taped 13mm Hot-Melt Seam Tape |
| Urban Tech / Windbreaker | 2.5-Layer (2.5L) Lightweight 50D Mechanical Stretch Polyester | 10,000 mm H2O | 10,000 g/m²/24hr | Critically Taped Seams + Laser Cut Vents |
| Softshell Athletic Jacket | 3-Layer Bonded Fleece: DWR Face + Mid-Layer TPU + Microfleece | 8,000 mm H2O | 5,000 g/m²/24hr | Flatlock Reinforced Seams + DWR Thread |
| Performance Activewear Sets | 75% Recycled Nylon / 25% Spandex High-Gauge Interlock Knit | Water-Resistant Finish (DWR) | High Air Permeability | 4-Needle 6-Thread Flatlock Seamless Stitching |
| Insulated Winter Parka | 300D Heavy-Duty Oxford Polyester + GRS Certified Recycled Down/Fill | 15,000 mm H2O | 8,000 g/m²/24hr | Baffle Wall Construction + Fully Taped Outer Shell |
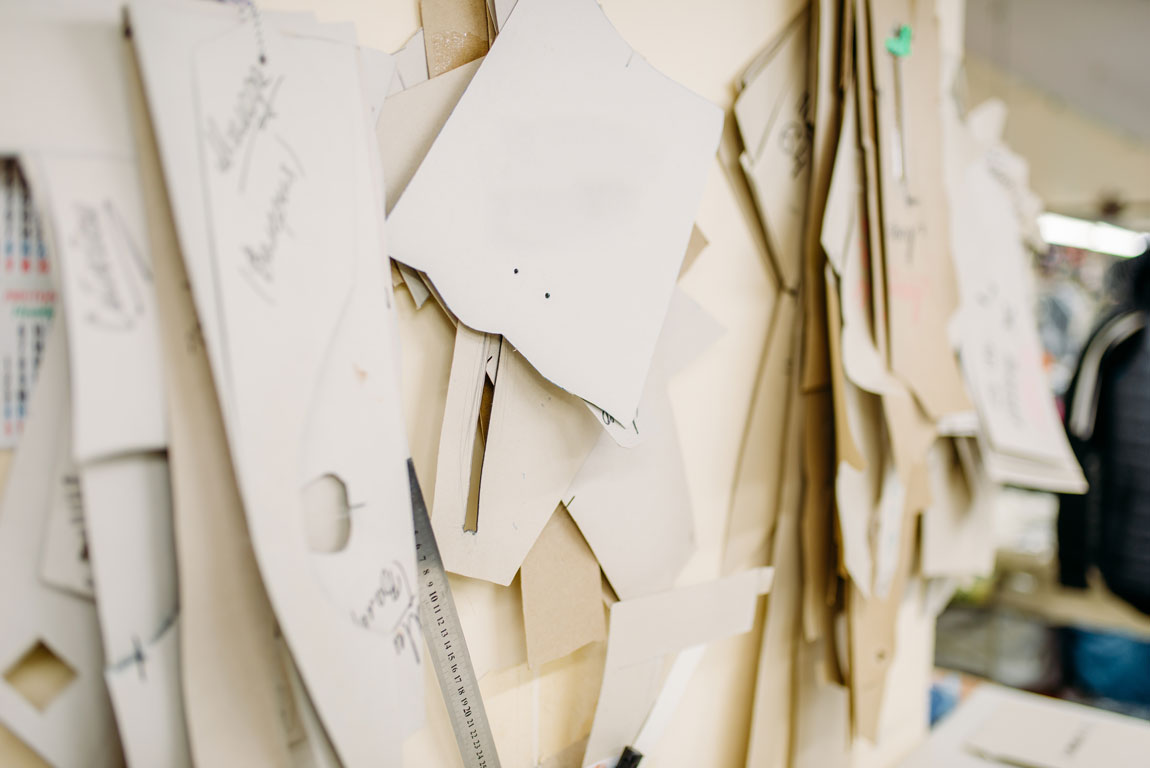
Our computerized Gerber CAD systems optimize pattern yield, reducing fabric waste by up to 14%. We grade sizes accurately across US, EU, and Asian fit standards to eliminate return rates.
Equipped with automated laser cutters, hot-air seam-sealing machinery, and programmable sewing stations capable of handling complex shell assembly, waterproof zippers, and custom pocket configurations.
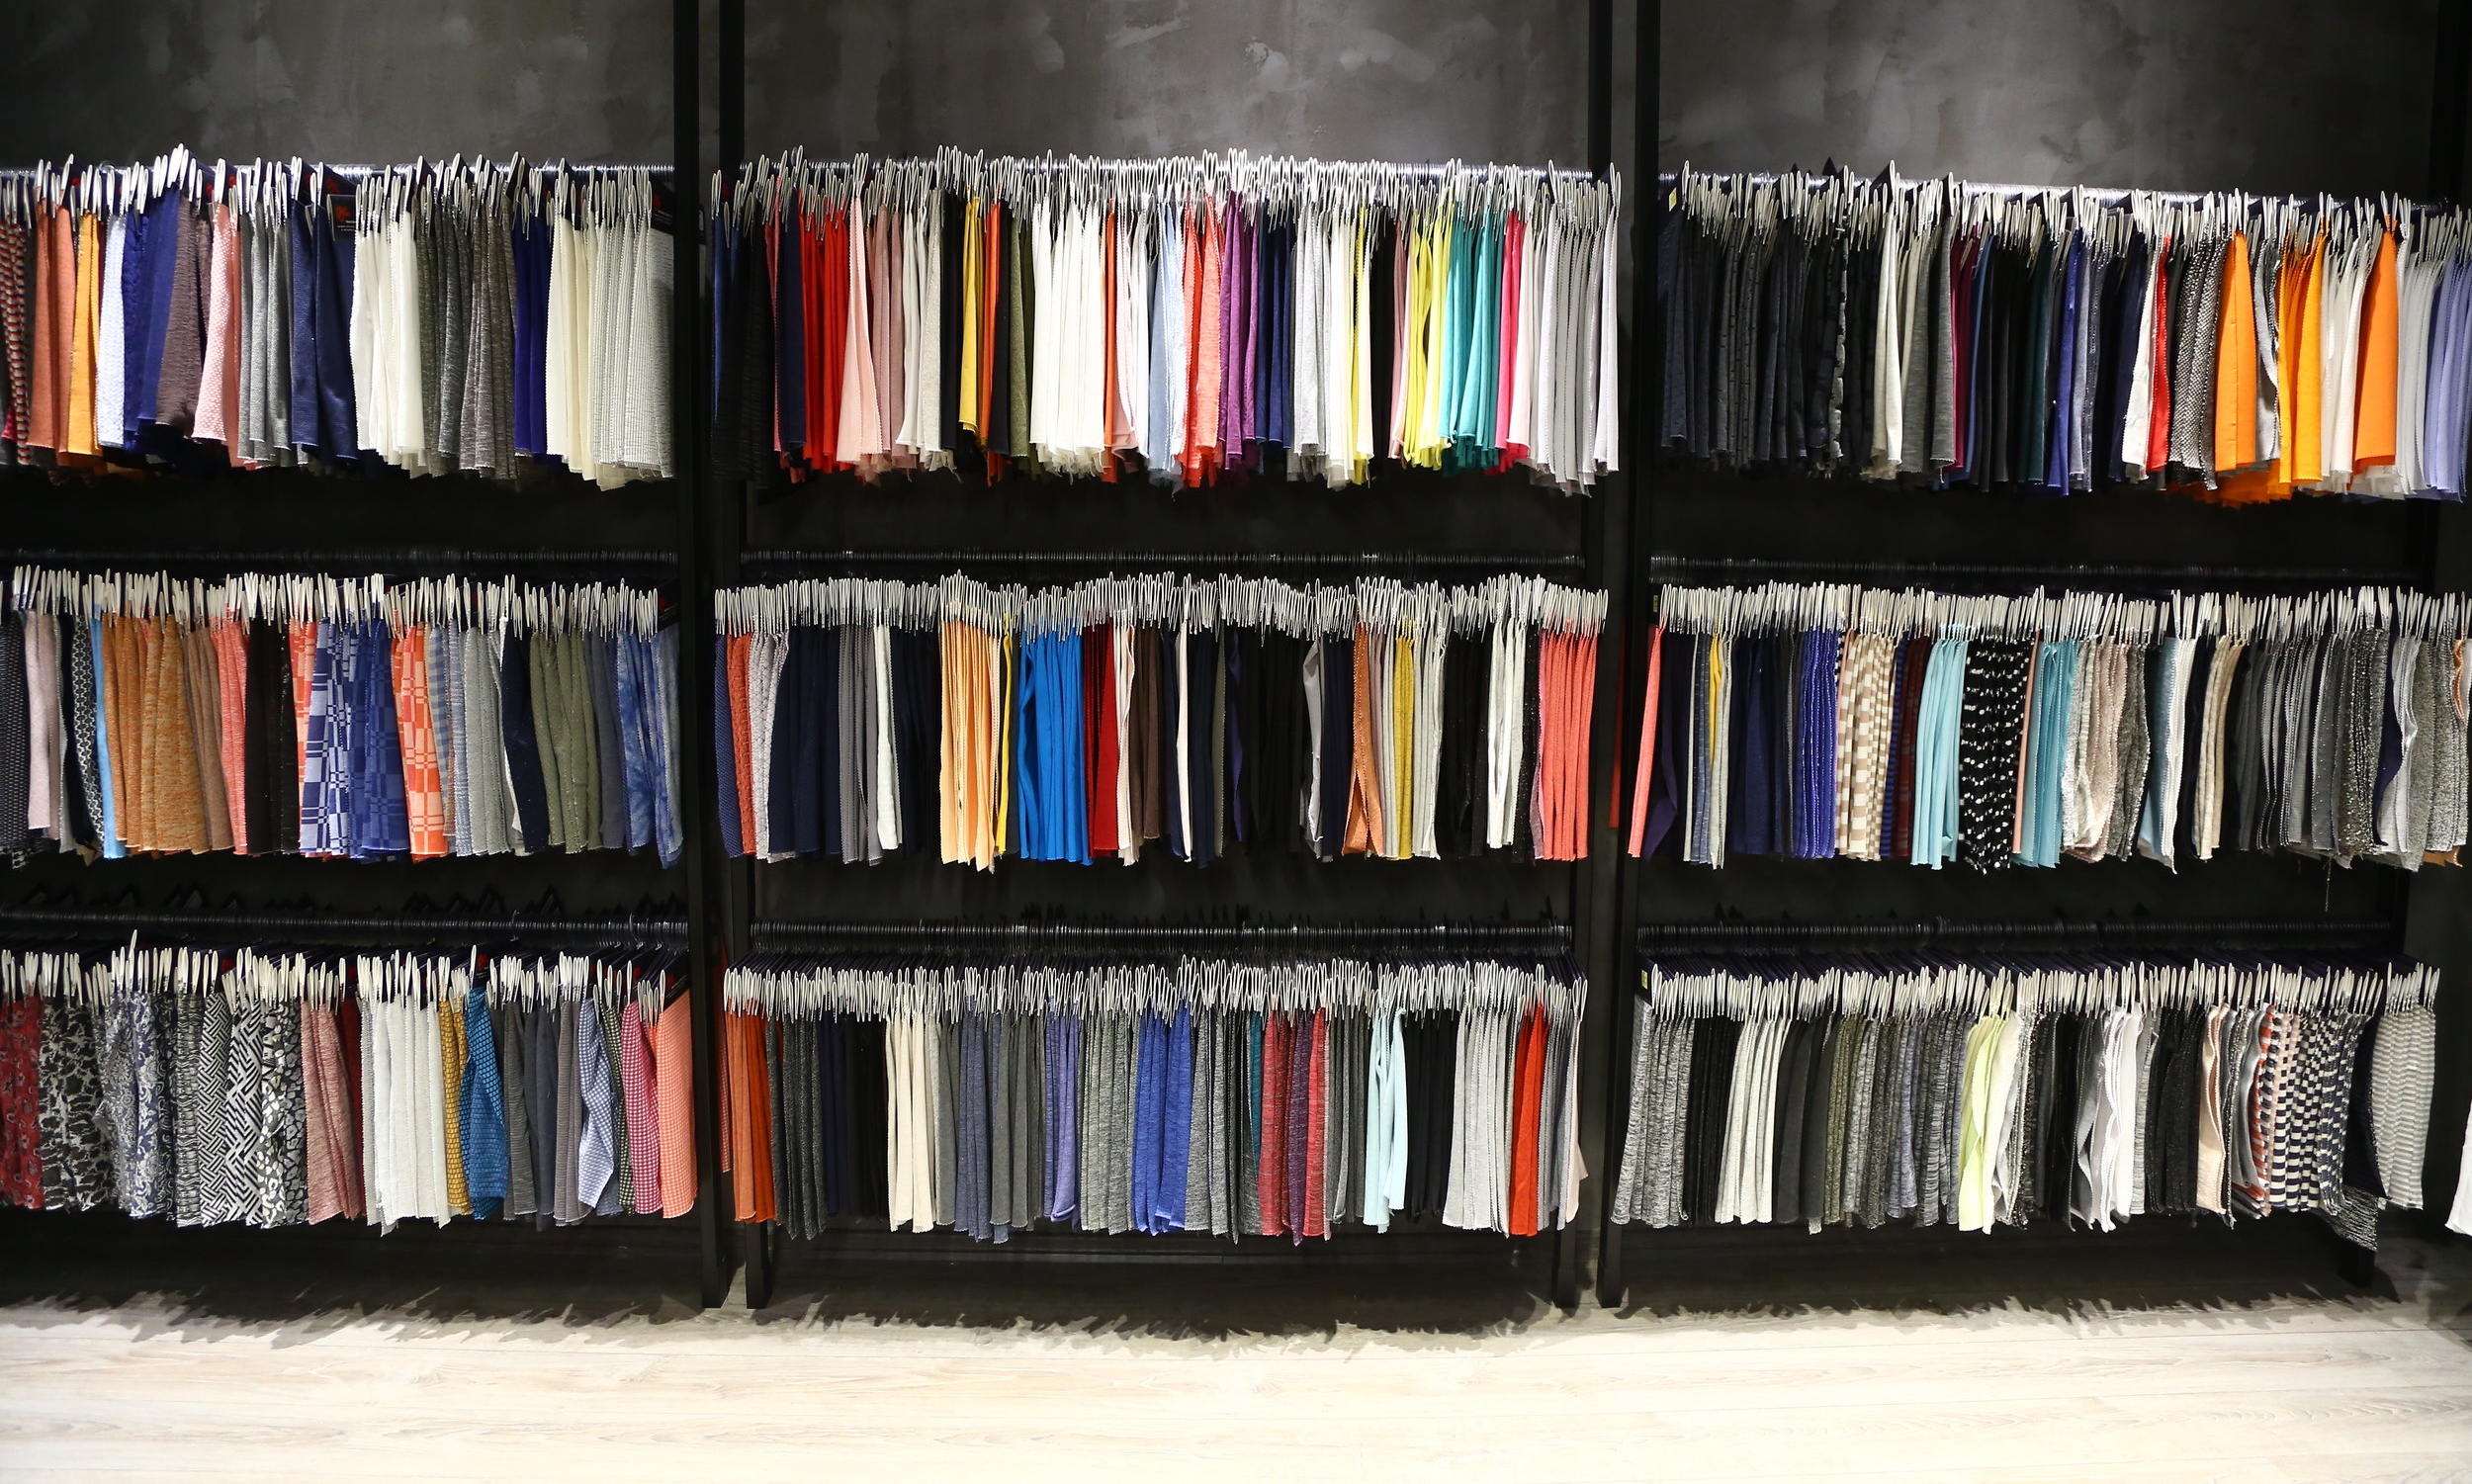
Direct partnerships with top textile mills give us priority access to bluesign® and OEKO-TEX® certified recycled polyesters, YKK waterproof zippers, Cordura® reinforcements, and custom metal hardware.
Transform wholesale blanks or custom-developed prototypes into market-ready retail products with our premium embellishment ecosystem.
High-density stitching for outerwear logos, chest patches, and headwear using colorfast Tajima machines.
High-stretch TPU heat seal transfers engineered for elastane activewear and storm-flap jacket branding.
Water-based discharge printing and full-bleed dye sublimation that maintains fabric breathability and soft hand-feel.
Custom woven main labels, FSC-certified hangtags, barcode polybagging, and retail-ready carton packing.
Consult directly with our textile engineering team for mill-direct custom pantone dyeing, moisture-wicking coatings, and membrane bonding.
From initial tech pack review to final container loading—how we safeguard quality at every milestone.
Review tech packs, digitize patterns, establish bill of materials (BOM), and calculate precise yield costings.
Construct 1st Proto sample in 7-10 days for fit validation, seam stress testing, and fabric hand-feel approval.
Pantone color matching under D65 light boxes, strike-off prints, zipper pull customization, and trim approvals.
Automated cutting, line assembly, inline seam-taping inspection, and hydrostatic pressure quality audits.
Final needle detection, AQL 2.5 visual/functional inspection, custom export packaging, and global freight dispatch.
To guarantee that high-altitude jackets and extreme activewear perform reliably in real-world conditions, all fabric batches undergo rigorous third-party and in-house laboratory testing prior to cut-and-sew operations.
Direct answers to common questions asked by supply chain managers, brand directors, and apparel buyers.
Our standard MOQ for custom technical outerwear (jackets, parkas, windbreakers) starts at 300 pieces per design/colorway depending on fabric custom dyeing requirements. For activewear sets using stock-supported stretch fabrics, we can accommodate lower initial orders of 100 to 200 pieces to support emerging brands.
While complete Tech Packs with spec sheets accelerate sampling, our Los Angeles R&D team can transform high-resolution reference photos, physical garment samples, or design sketches into full vector tech packs, pattern grading charts, and 3D digital simulations.
Every waterproof outerwear order utilizes hot-melt seam-taping machinery calibrated for specific membrane melting points. We perform inline hydrostatic pressure testing on taped seams every 50 units during production to ensure zero water penetration at 10,000mm+ H2O pressure.
Physical sample development takes 7 to 12 business days upon tech pack confirmation. Bulk production lead times generally range from 25 to 35 days after pre-production sample (PPS) approval, supported by expedited air or sea freight arrangements.
Yes. Our network includes GRS (Global Recycled Standard), OEKO-TEX® Standard 100, and bluesign® certified fabric suppliers. We provide full transaction certificates (TC) for recycled polyester/nylon claims and adhere to BSCI and ISO9001 factory audit protocols.
We execute strict legally binding Non-Disclosure Agreements (NDAs) prior to tech pack review. Your custom patterns, tech packs, and brand graphics remain 100% confidential and are never shared, sold, or repurposed for third-party production.
Partner with China's leading technical outerwear development manufacturer. Gain instant access to our fabric library, rapid prototyping line, and competitive factory-direct pricing structures.