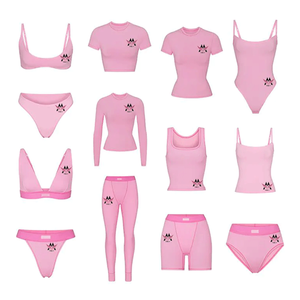
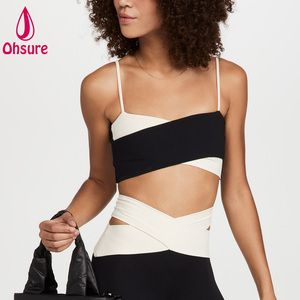
Direct Factory Sourcing Solutions with Low MOQ & Full Private Label Customization
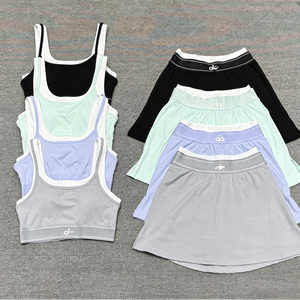
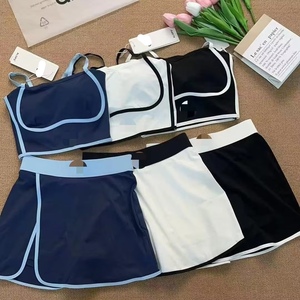
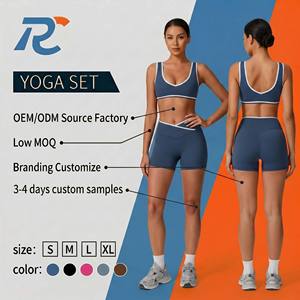
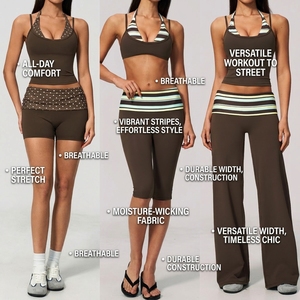
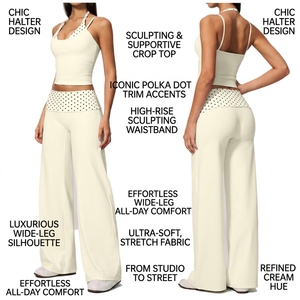
Combining Cut & Sew Precision with Technical Unboxing Excellence
From custom tech packs, pattern grading, marker making, to computerized fabric cutting and automated stitching lines, our factory facilities support complex athletic activewear, compression sets, and luxury street apparel.
We eliminate supply chain fragmentation by providing direct integration of custom frosted TPU ziplock polybags, GRS-certified recycled mailers, rigid magnetic gift boxes, custom woven labels, and FSC-certified hangtags directly at the apparel production line.
Every piece of clothing and packaging unit undergoes strict multi-stage inspection including tensile strength testing, seam pull stress evaluation, colorfastness validation, barcode scannability checks, and eco-compliance verification.
In the contemporary fashion and activewear ecosystem, the packaging is no longer merely a protective transport envelope; it serves as the first physical touchpoint of customer brand experience and a critical vector for supply chain efficiency. Modern clothing manufacturers in China have evolved beyond simple textile assembly. By integrating specialized custom packaging directly into the primary manufacturing process, brands eliminate secondary logistics handling, cut lead times by up to 25%, and significantly reduce transit damage.
Whether producing high-stretch seamless yoga sets, moisture-wicking compression bras, or custom-embossed activewear, pairing premium garments with high-performance packaging elevates perceived retail value. Direct-to-consumer (D2C) brands and global wholesale distributors alike leverage custom packaging to communicate sustainability commitments, prevent environmental degradation during ocean or air transport, and ensure pristine presentation upon unboxing.
As international trade regulations tighten regarding single-use plastics and Extended Producer Responsibility (EPR) mandates take full effect across global markets, China's leading garment packaging factories are pioneering systemic innovations. Understanding these macro trends allows sourcing directors and apparel brand owners to future-proof their supply chain strategies.
The global shift toward net-zero manufacturing has accelerated the adoption of next-generation bio-based polymers and ocean-bound plastic recovery. Traditional low-density polyethylene (LDPE) packaging is rapidly being replaced by bio-resins that decompose naturally within 180 days under industrial composting conditions without leaving toxic microplastic residues. Furthermore, water-soluble garment bags made from polyvinyl alcohol (PVA) are setting new benchmarks for zero-waste packaging in hydrophobic activewear delivery.
Modern fashion logistics requires complete real-time visibility from factory floor to end consumer. Incorporating flexible RFID labels directly into heat-sealed garment packaging allows automated scanning of multi-item boxes at distribution hubs without manual unpacking. This smart integration reduces order processing errors by over 90% while providing consumers with instant digital authentication of organic cotton or recycled polyester garment origin via smartphone NFC interaction.
With global freight costs subject to volatility, volume optimization has become a dominant cost-reduction driver. Advanced clothing factories utilize automated micro-vacuum sealing technologies for bulk activewear and outerwear shipping. By removing excess air from padded sports bras, plush hoodies, and multi-piece tracksuits, packaging volume is compressed by 35% to 50%, dramatically maximizing container load factors and lowering per-unit carbon footprint.
Sourcing strategies are shifting from fragmented, multi-vendor procurement to consolidated single-source enterprise partnerships. Brands historically sourced raw garments from one mill, woven labels from a second supplier, and printed shipping bags from a third. This traditional model resulted in severe communication friction, mismatched lead times, color consistency failures, and heightened risk of supply chain disruption.
Leading Chinese manufacturers now offer vertical end-to-end management: raw yarn spinning, circular knitting, dyeing, cut & sew assembly, custom brand packaging, and direct door-to-door Amazon FBA or 3PL fulfillment.
To mitigate inventory markdowns, brands require agile batch production. Modern factories support low MOQ custom runs starting as low as 100-300 pieces per style with 7-day rapid physical sample prototyping.
Using computerized spectrophotometers and automated camera vision systems, factories guarantee 100% color matching accuracy between custom-dyed activewear fabrics and custom-printed packaging trims.
Our manufacturing complex combines 20+ years of activewear development expertise with cutting-edge packaging design and printing technologies. Located at the epicenter of China’s textile and industrial design hubs, we empower sportswear brands, fitness apparel startups, and corporate clients to achieve market dominance.
We provide highly flexible procurement structures. Standard custom activewear production starts at low MOQs of 100 to 300 sets per colorway, while custom printed polybags and hangtags start at 500 to 1,000 units. Bulk volume discounts automatically apply for higher tier production runs.
Yes. We offer fully certified GRS 4.0 100% post-consumer recycled (PCR) plastics, 100% biodegradable PLA/PBAT compostable mailers, and FSC-certified recycled paper boxes complete with official transaction certificates (TC) for customs verification.
All clothing items undergo anti-moisture processing and are packed inside sealed, anti-fungal polybags containing non-toxic food-grade silica desiccant packs. Micro-ventilation holes are designed with anti-dust flap valves to block ocean humidity.
Absolutely. Our experienced engineering team can create full 2D/3D tech packs from initial design sketches or reference samples. We provide physical pre-production samples—including fully printed custom packaging—for final client sign-off prior to bulk production.
We support high-definition rotogravure printing, flexographic eco-inks, offset lithography, UV spot gloss, metallic foil stamping, embossed/debossed logos, and high-contrast digital barcoding for maximum visual impact and scannability.
Sample creation generally takes 7 to 10 business days upon artwork confirmation. Bulk production of apparel and integrated packaging is typically completed within 15 to 25 business days depending on order complexity and total volume.
Connect with our senior technical engineers today to request custom quotes, fabric swatches, and eco-packaging sample kits.
Contact Us