The Strategic Ecosystem of China's Sleepwear & Loungewear Production
Navigating the global sleepwear market requires more than standard vendor selection—it demands an intimate understanding of raw material engineering, regional industrial clusters, and precision technical manufacturing. As a premier full-service apparel manufacturer operating at the center of China’s textile clusters (Guangdong, Zhejiang, and Jiangsu), our production matrix delivers high-precision OEM and ODM capabilities tailored specifically for DTC brands, premium boutique labels, and enterprise-scale importers.
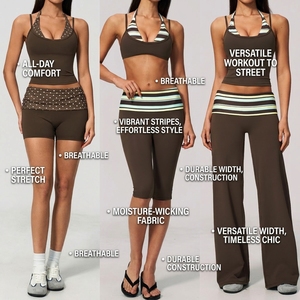
Modern sleepwear has expanded far beyond traditional nightgowns and pajamas. The rise of "Sleep-to-Street" active-loungewear hybrids has accelerated consumer expectations regarding tactile soft touch, thermal regulation, fabric breathability, and garment durability. Meeting these demands requires seamless integration between raw fiber sourcing, circular knitting or weaving technologies, and sophisticated cut-and-sew craftsmanship.
Pure Mulberry Silk Engineering
Sourced directly from Zhejiang and Jiangsu silk weaving mills, our pure 6A grade Mulberry silk sleepwear ranges from 19 to 30 momme (MM). We utilize eco-friendly reactive dyeing techniques that preserve silk's natural sericin protein layers, preventing skin friction while delivering natural hypoallergenic and thermoregulating properties.
TENCEL™ Modal & Bamboo Viscose
For high-volume eco-conscious nightwear lines, we process certified Austrian Lenzing TENCEL™ Modal (Micro 80s/100s yarn count) and organic bamboo viscose. These fibers provide superior moisture absorption (50% higher than cotton), silky drapability, resistance to pilling, and exceptional dimensional stability after repeated laundering.
Seamless & 4-Needle 6-Thread Construction
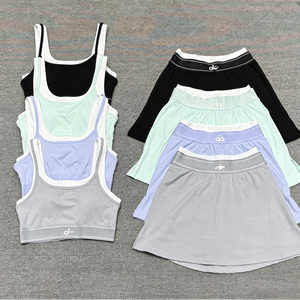
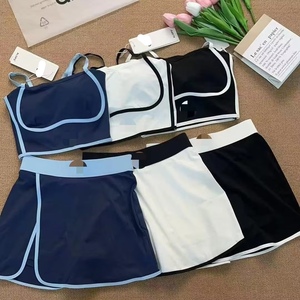
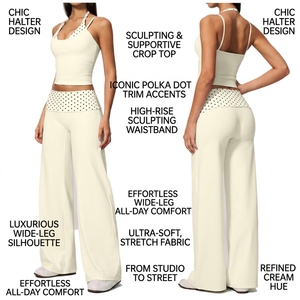
Utilizing SANTONI circular seamless knitting machines and ISO 607 flatlock stitching, our factory manufactures active-loungewear and pajama sets that minimize skin abrasion. Elastic waistbands are engineered with encased plush elastic or soft fold-over bands to deliver zero-pressure luxury fit profiles.
Technical Benchmarking
Sleepwear & Nightwear Fabric Selection Matrix
Selecting the optimal fabric composition is the cornerstone of private label profitability and customer retention. Review our standard technical specifications below:
Future Sourcing & Procurement Trends in Private Label Sleepwear
As consumer preferences shift toward holistic wellness and ethical manufacturing, the private label sleepwear industry is undergoing structural transformations. Sourcing executives and brand founders must align with modern operational strategies to maintain margin dominance and brand authority.
1. Smart Functional & Bio-Infused Textiles
The next decade belongs to sleepwear that actively enhances physiological recovery. Our R&D division works with mills to integrate microencapsulated wellness agents—such as Aloe Vera, Vitamin E, and Far-Infrared (FIR) emitting minerals—directly into fabric yarns. These bio-functional sleep garments promote skin hydration and circulation during rest.
2. 3D Digital Sampling & Rapid Prototyping
To reduce sampling lead times from weeks to days, our design facilities utilize CLO3D virtual garment rendering. Private label clients can review physical drape, tension maps, print placement, and colorways in true-to-life 3D digital environments before a single piece of fabric is cut, dramatically accelerating time-to-market.
3. Low-MOQ Agile Supply Chains
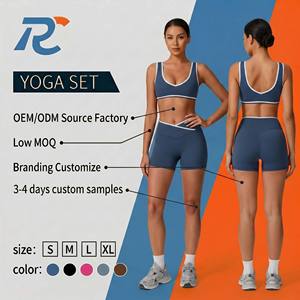
Inventory overstock remains the largest margin destroyer in apparel retail. We offer agile manufacturing modules that support low Minimum Order Quantities (MOQs starting from 100-200 pieces per style), backed by raw fabric greige holding agreements that allow rapid re-order replenishment within 10 to 14 business days.
Operational Capabilities
Full-Service Private Label & Cut & Sew Infrastructure
From raw yarn sourcing to final packaged delivery, our end-to-end manufacturing ecosystem eliminates intermediary markups and guarantees total quality control.
Pattern Making & Tech Packs
Our master pattern makers translate sketch concepts, mood boards, or physical samples into digital CAD grading files. We build fully detailed technical packages specifying stitch types, seam allowances, tolerance charts, and trim placements to guarantee absolute consistency across size runs (XS through 5XL).
Custom Branding Applications
Transform blank apparel into high-value brand assets. Our decorative applications include precision high-density 3D embroidery, satin piping finishes, eco-friendly water-based screen printing, silk sublimation, heat-transfer neck labels, and custom woven brand tags.
AQL 1.5/2.5 Strict Quality Assurance
Every batch undergoes multi-stage inspections complying with international Acceptable Quality Limit (AQL) 1.5/2.5 standards. Inspections include raw fabric needle detector scanning, shade sorting, seam strength pull-testing, dimensional stability washing tests, and final retail-ready polybag audit packing.
Direct technical answers to common questions asked by global apparel sourcing directors, brand owners, and inventory buyers.
Q:
What is the standard Minimum Order Quantity (MOQ) for custom private label sleepwear?
Our baseline flexible MOQ starts at 100 to 200 pieces per style/colorway for garments using stock greige fabrics (such as standard TENCEL™ Modal, bamboo viscose, or cotton blends). For custom yarn-dyed plaid sleepwear, custom pantone fabric dyeing, or specialized luxury Mulberry silk, the typical MOQ is 300 to 500 pieces per order. We also offer multi-size distribution options within each batch.
Q:
How do you ensure eco-friendly compliance and international fabric certifications?
All raw fabrics processed in our factories are certified under OEKO-TEX Standard 100 (Class I), guaranteeing freedom from harmful azo dyes, formaldehyde, and heavy metals. For organic sleepwear lines, we provide GOTS (Global Organic Textile Standard) transaction certificates, as well as FSC-certified Lenzing TENCEL authentication documentation upon contract execution.
Q:
What is the typical production timeline for sample development and bulk manufacturing?
Standard prototype sample lead time requires 5 to 7 business days following tech pack and fabric approval. Bulk cut-and-sew manufacturing typically requires 15 to 25 calendar days depending on style complexity and branding embellishments. Air freight dispatch takes 3-5 days globally, while sea freight logistics range from 18 to 30 days depending on the destination port.
Q:
Can your factory accommodate custom sizing systems for international markets?
Yes. We possess extensive pattern grading experience across North American, European, Australian, and Asian fit standards. Whether your target demographic requires US standard sizing, UK relaxed loungewear fit, or inclusive Plus-Size (up to 5XL) ergonomic grading, our computerized CAD pattern grading systems execute precise size expansion with zero distortion to garment proportions.
Q:
What custom branding accessories and retail packaging solutions do you provide?
We provide full turn-key private labeling package services including custom woven main neck labels, printed satin wash care labels, FSC recycled paper hangtags with custom foil stamping, custom branded frosted zip-lock polybags, tissue paper wrapping, and custom corrugated shipping boxes ready for direct fulfillment center intake.
Q:
How are fabric shrinkage and color fastness controlled in nightwear production?
Every fabric batch undergoes pre-shrunk steam tumbling and heat setting treatments prior to laser or manual cutting. We guarantee a wash shrinkage rate of less than 3% to 4% under standard home laundering conditions. Color fastness to laundering, rubbing, and light exposure is lab-tested to meet ISO 105 / AATCC Grade 4-5 standards.
Ready to Launch or Scale Your Private Label Sleepwear Brand?
Partner with China's leading OEM/ODM apparel factory. Request our master fabric swatches, technical catalog, and instant wholesale manufacturing quotation today.