Explore our exporter-grade sample catalog engineered with premium surface treatments, ergonomic pattern engineering, and advanced moisture-wicking garment finishing.
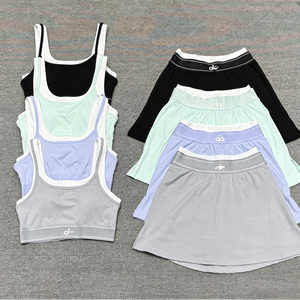
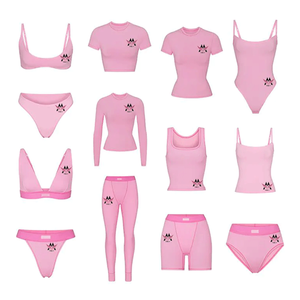
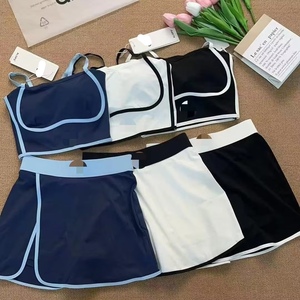
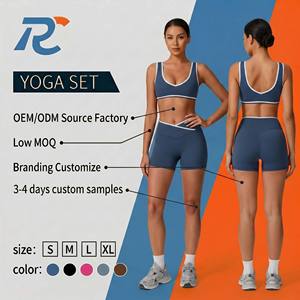
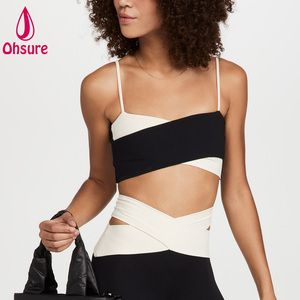
As a premier global exporter specializing in cut & sew production, private label development, and full-spectrum garment finishing, our operations bridge the gap between architectural apparel design and high-volume retail delivery.
Garment finishing is the critical qualitative bridge that converts raw assembled textiles into high-margin, commercial-ready apparel. Beyond basic cutting and sewing, professional finishing encompasses chemical treatments, mechanical surface modifications, thermal setting, anti-microbial coatings, precision pressing, and strict export-level packaging.
Our state-of-the-art facilities integrate flexible low-MOQ capabilities with high-capacity automated finishing lines, accommodating luxury fashion houses, activewear labels, corporate chains, and boutique global brands with equal efficiency.
An engineering perspective on wet, dry, and functional garment finishing processes deployed for export apparel.
Engineered silicone softening, bio-enzyme wash, ozone bleaching, micro-emulsion conditioning, and reactive garment dyeing designed to elevate hand-feel and dimensional fastness.
Hydrophilic quick-dry treatments, silver-ion antibacterial coatings, UPF 50+ UV blockers, anti-static encapsulation, and durable water repellent (DWR) C0 nano-coatings.
Peach-skin suede sanding, zero-tension calendering, shearing, laser distressing, and tunnel-steamer tension removal to control post-wash shrinkage under 2.5%.
3D puff embroidery, high-density screen printing, sublimation transfer, silicone heat press labels, custom metal hardware attachment, and retail-ready kitting.
| Finishing Method | Primary Technical Objective | Target Fabric Types | Durability Rating | Eco/Sustainability Impact |
|---|---|---|---|---|
| Silicone Micro-Emulsion | Extreme silk-touch hand-feel & elastane recovery | Cotton/Spandex, Nylon Activewear | 30+ Washes | OEKO-TEX Class 1 Compliant |
| Ozone Eco-Washing | Waterless pigment reduction & vintage wash effect | Denim, Heavy French Terry | Permanent | 95% Water Savings |
| Hydrophilic Nano-Finish | Moisture management & rapid evaporative cooling | Polyester Seamless Knit, Active Tops | 50+ Washes | Fluorine-Free (PFC-Free) |
| Tensionless Tunnel Steaming | Relaxation of knitting tension & warp stabilization | Viscose, Ribbed Knits, Activewear | Permanent | Zero Chemical Usage |
| C0 Non-Fluorinated DWR | Water & stain repellency without toxic PFCs | Outerwear Shells, Track Jackets | 20+ Washes | 100% Biodegradable |
Leveraging full in-house capabilities to streamline apparel prototyping, trim sourcing, cut-and-sew, and final export finishing under one single-source agreement.
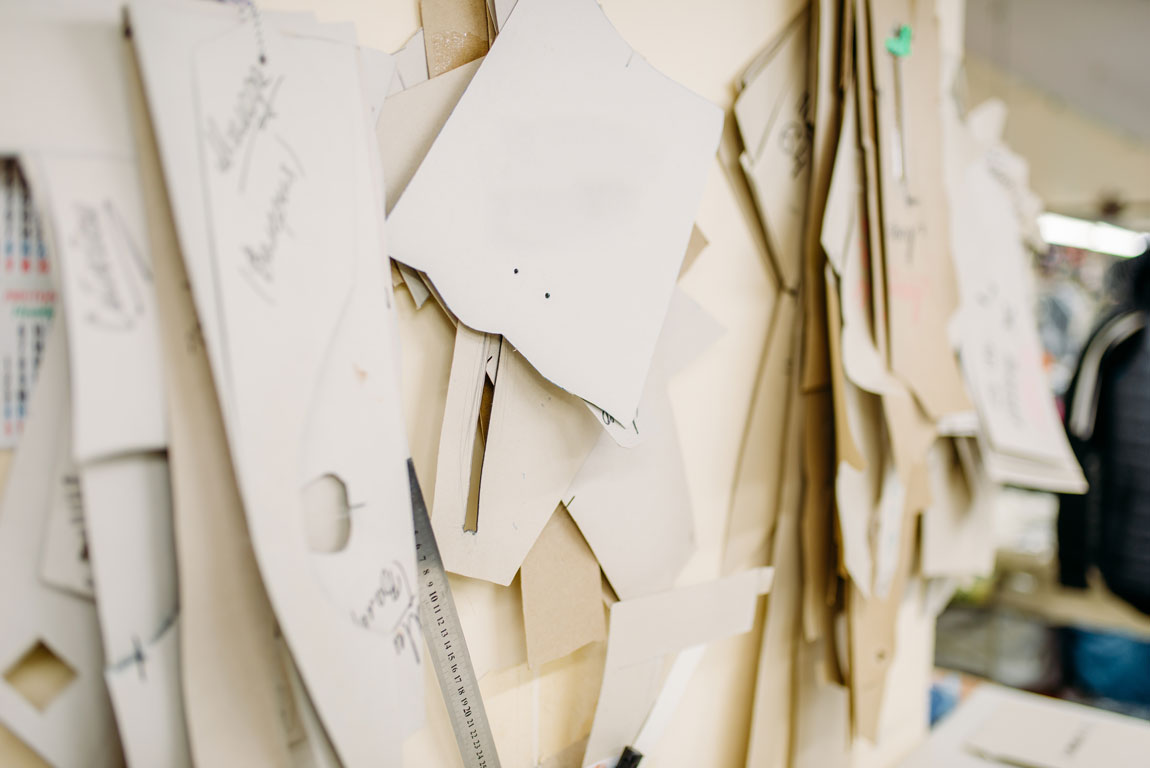
Flawless finishing begins long before garments enter the dye vat or washing steam tunnel. Our specialized OEM/ODM workflow integrates computer-aided pattern design (CAD), grading for global size standards (US/EU/Asia), and automated marker making to minimize fabric waste.
Our sample development teams test fabric shrinkage behavior under specific finishing temperatures during prototype stages, ensuring that finished garments align precisely with technical spec sheets down to the millimeter.
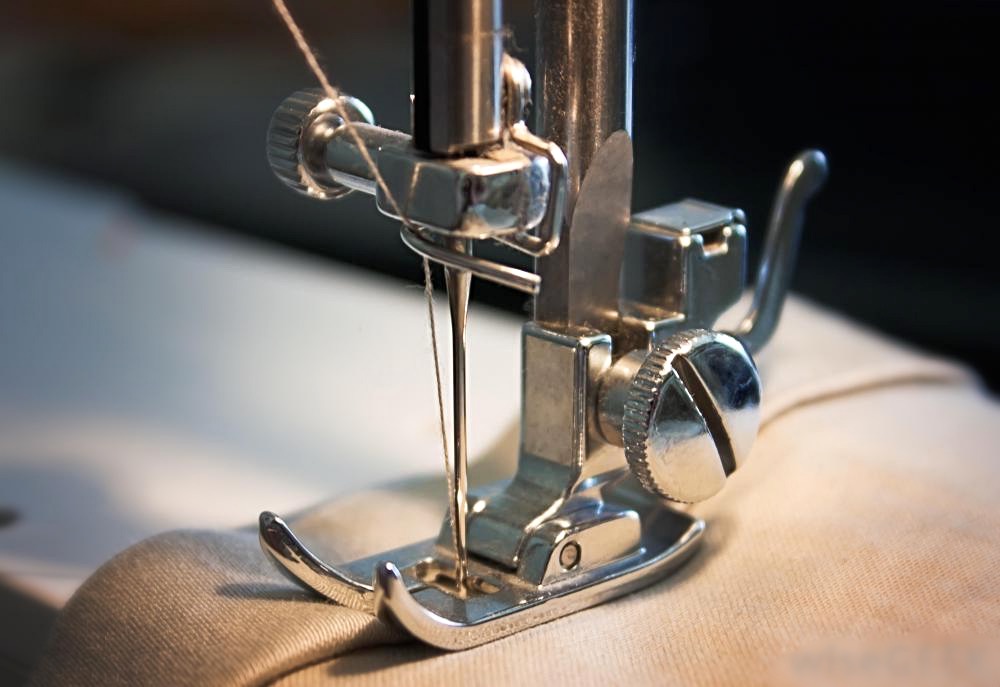
With high-speed automated cutting tables and specialized sewing machinery (4-needle 6-thread flatlock, coverstitch, overlock, and lockstitch), we produce high-durability apparel ready for intensive post-assembly finishing treatments.
Every seam is structuralized to withstand mechanical washing stress, enzyme abrasion, and industrial steam pressing without thread popping or seam puckering.
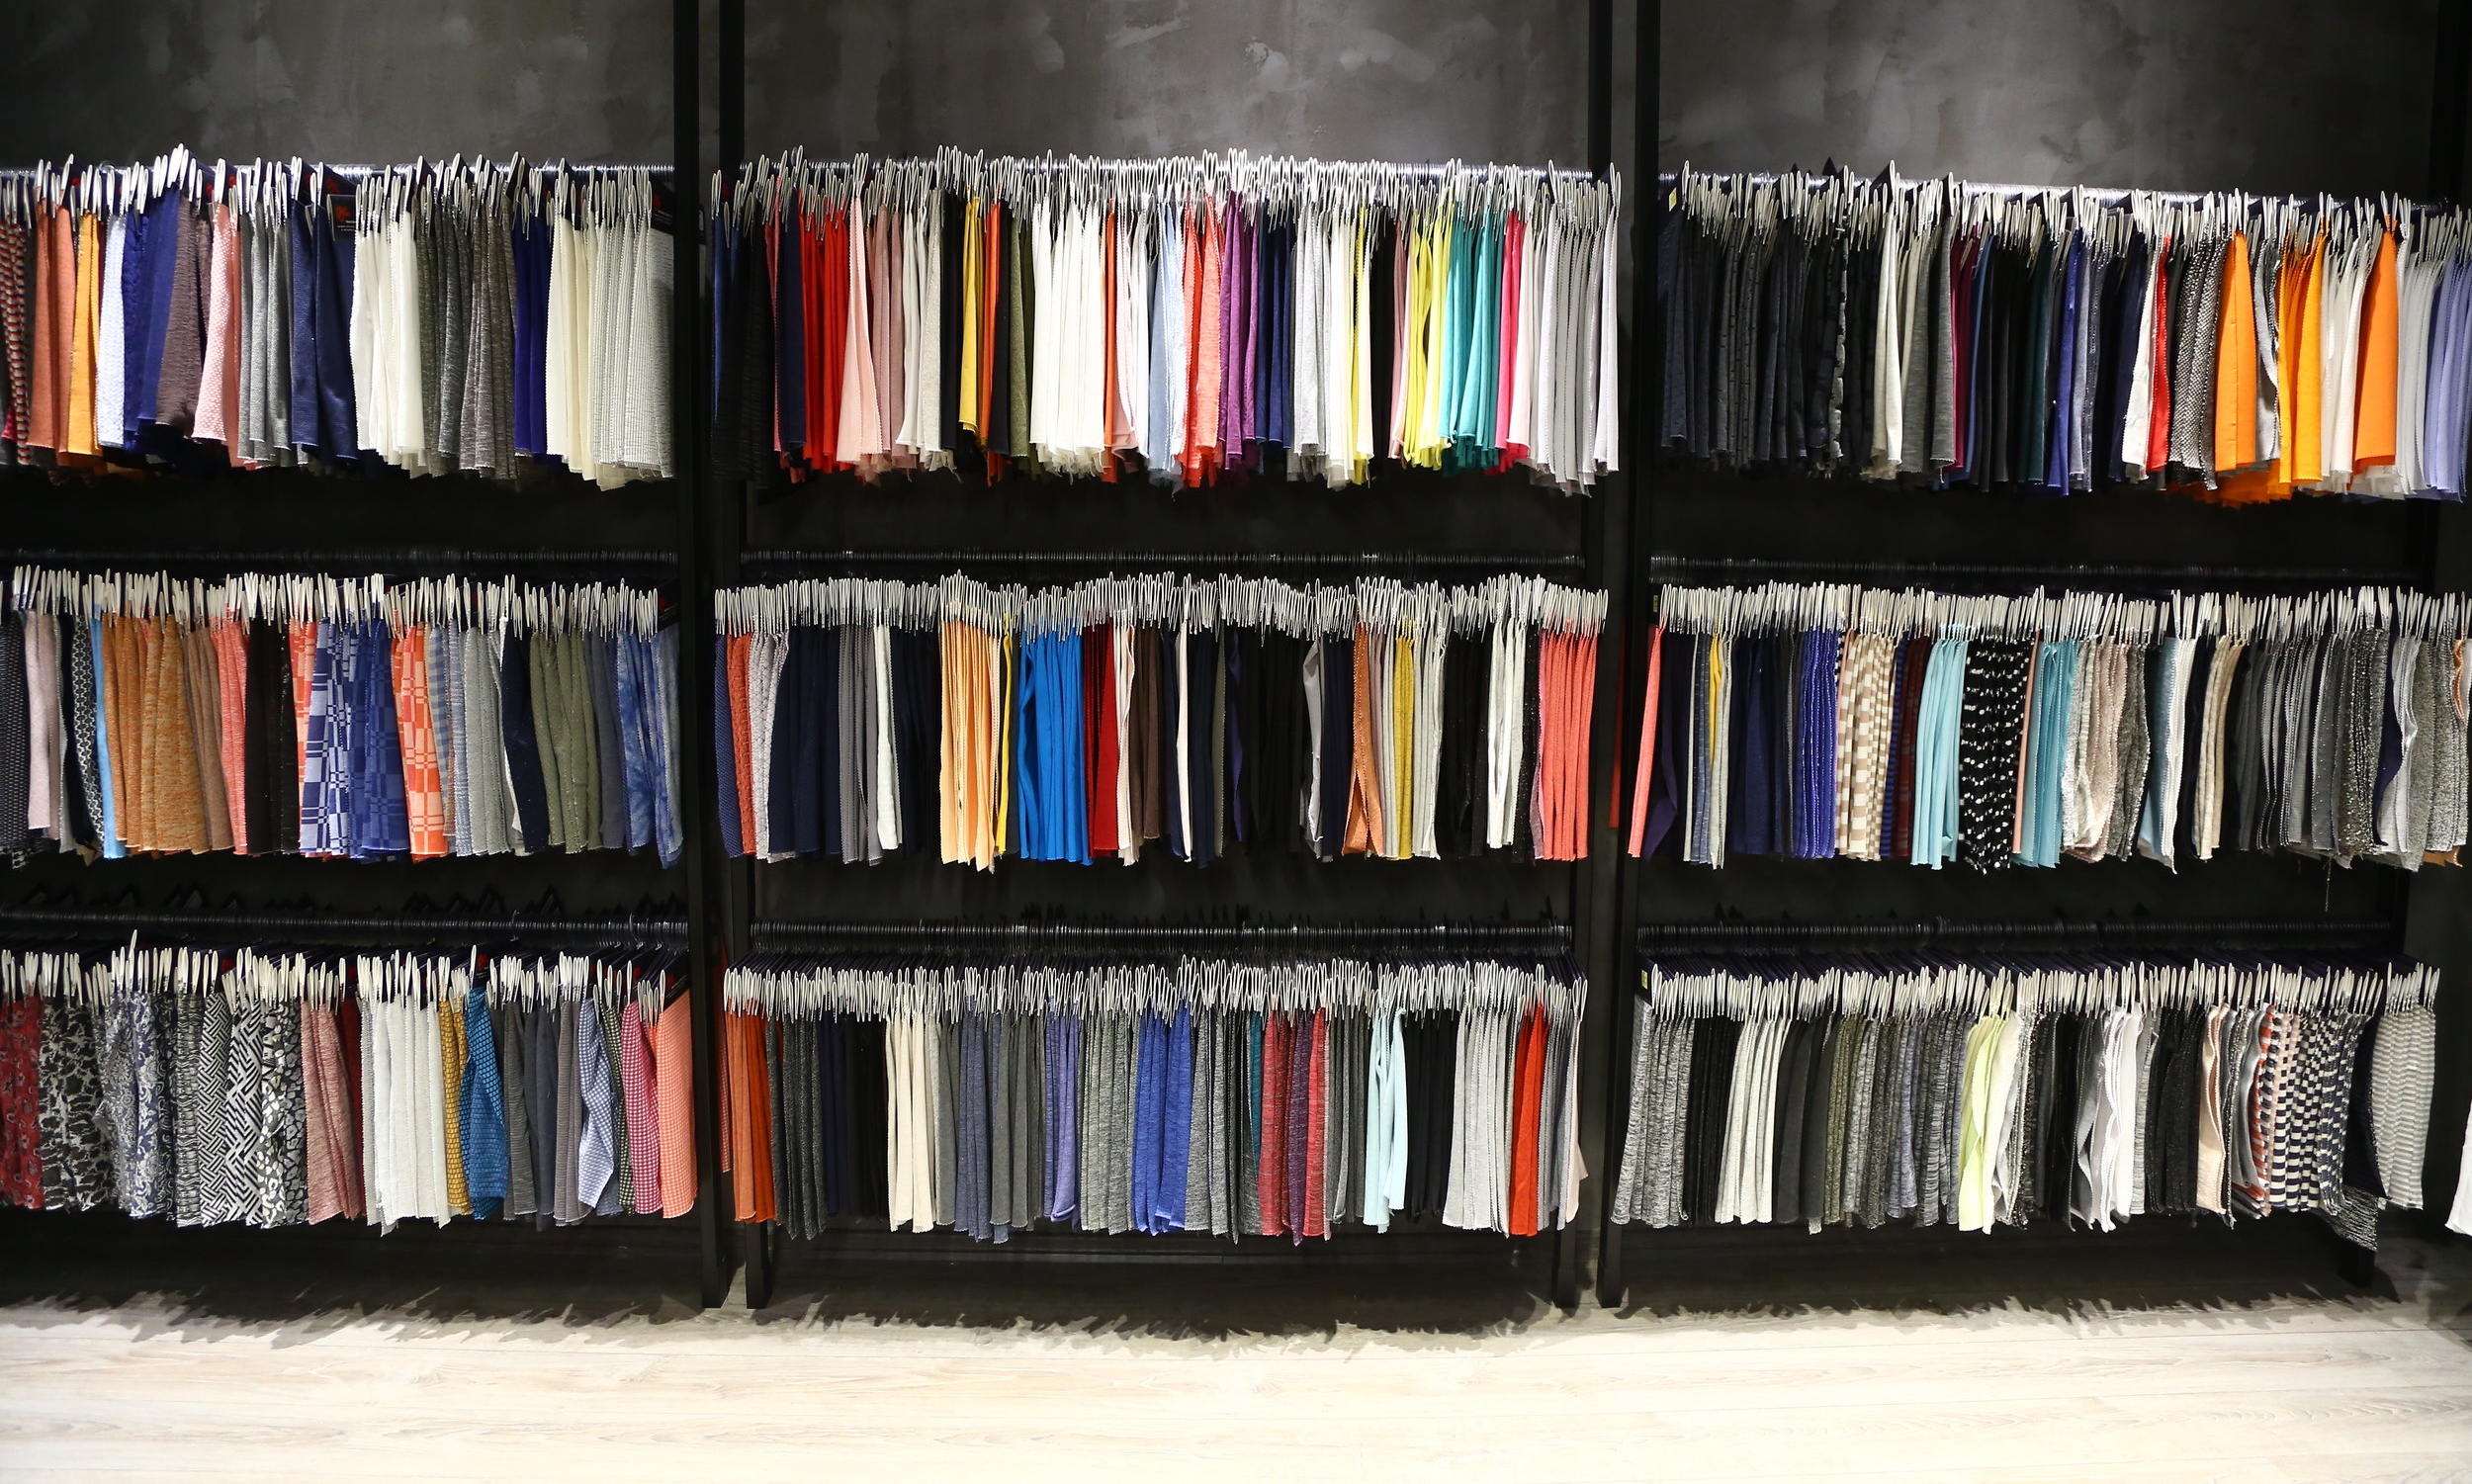
Access over 100+ vetted textile mills and trim suppliers worldwide. Whether sourcing GOTS-certified organic cotton, recycled REPREVE® polyester, high-gauge elastane knits, or specialized functional zippers and heat-transfer films, our procurement infrastructure handles complete raw material management.
Strategic market intelligence for global buyers, brand directors, and supply chain managers preparing for 2026-2030 regulatory and consumer shifts.
The global garment finishing market is undergoing a seismic transition driven by three mega-forces: stringent European Union Ecodesign for Sustainable Products Regulations (ESPR), consumer demand for ultra-soft performance activewear, and digital supply chain transparency mandates. Importers rely heavily on exporters capable of low-carbon finishing and certified chemical safety.
Traditional wet finishing accounts for nearly 20% of global industrial water pollution. Modern OEM/ODM exporters are rapidly scaling waterless and low-liquor finishing alternatives:
Consumer expectations for activewear and athleisure have evolved beyond basic stretch. Future procurement trends focus on multi-functional finishes integrated into single-layer fabrics:
High interest rates and inventory holding costs have shifted procurement strategies from massive 10,000-piece bulk runs toward agile, low-MOQ repeat orders. Exporters equipped with modular finishing lines allow brands to place 300 to 500-piece test batches, rapidly scaling production based on real-time sell-through data.
Transforming basic pre-made or custom-manufactured garments into retail-ready collections with high-value imprinting and finishing details.
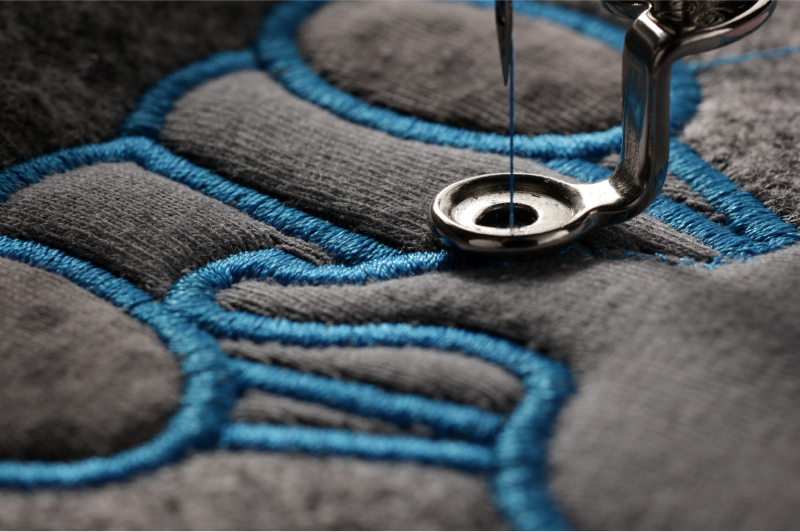
3D puff, flat, micro-embroidery, and applique execution with ultra-high stitch densities.
Water-based discharge, silicone ink, high-density print, and digital direct-to-garment options.
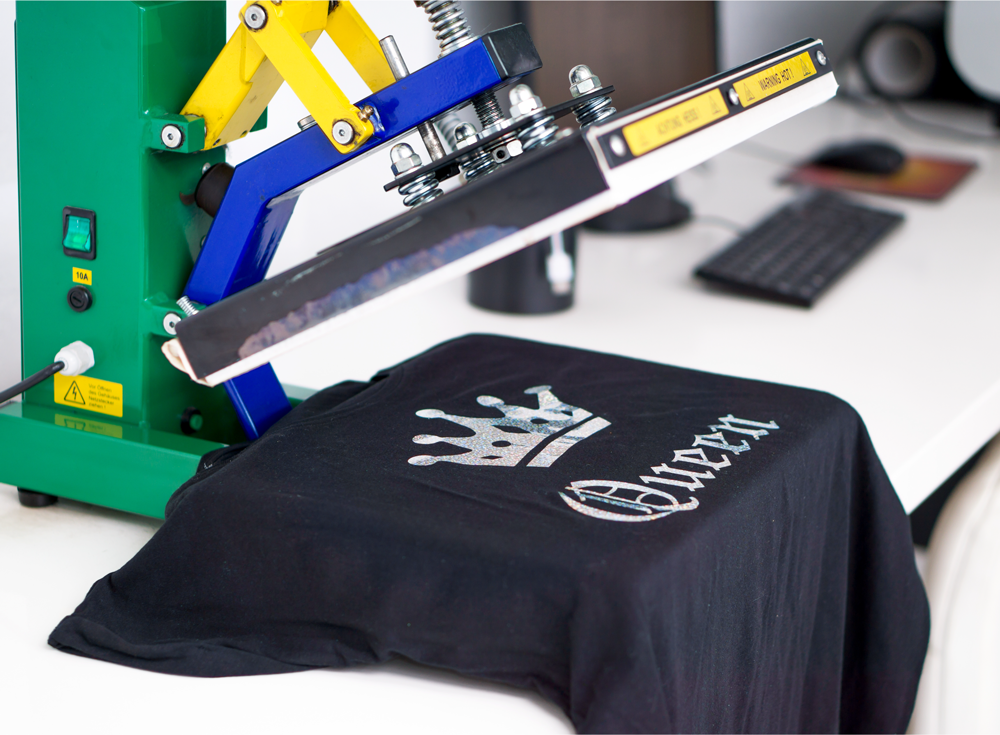
Reflective, metallic, flock, TPU, and stretch vinyl transfers engineered for high-wash durability.
Rigorous international testing protocols ensuring zero-defect export shipments under AQL 1.5 standards.
4-Point fabric inspection system analyzing GSM weight tolerance, color shading under D65 standard light, yarn defects, and elastane tension consistency prior to cutting.
Continuous visual and dimensional tracking at critical sewing stations. Verification of SPI (Stitches Per Inch), seam elasticity, and thread tension settings.
Laboratory testing for wash fastness (AATCC 61), crocking fastness (ISO 105-X12), formaldehyde content, pH balance (ISO 3071), and post-wash shrinkage percentages.
Garments undergo steam pressing, metal detection needle scans, folding, polybagging, barcode verification, and final AQL 1.5 random sampling before carton sealing.
Direct technical answers addressing global buyer intent, production workflows, and exporter protocols.
OEM (Original Equipment Manufacturer) Finishing: We execute your exact customized finishing specs, tech packs, and chemical formulas on garments built precisely to your proprietary design patterns.
ODM (Original Design Manufacturer) Finishing: We offer complete end-to-end solutions where our in-house development team provides pre-engineered apparel styles, fabric formulations, and curated finishing treatments that you can brand and export under your own label.
We utilize computerized spectrophotometer color matching (Datacolor systems) to maintain Delta E (ΔE) color difference values under 0.8 compared to Pantone standard swatches. Every dye lot is lab-dipped, submitted for buyer sign-off, and verified under standardized light booths (D65 daylight, TL84 store light, and CWF).
Our finishing plant and raw chemical formulations comply with OEKO-TEX® Standard 100 (Class 1 safe for infant skin), ZDHC (Zero Discharge of Hazardous Chemicals) Level 3 guidelines, REACH European chemical safety regulations, and GOTS (Global Organic Textile Standard) for organic line items.
We support flexible low-MOQ programs starting as low as 100 to 300 pieces per style/color for specialized private label lines, while scaling up to high-capacity bulk orders exceeding 50,000 pieces per month for major international retail chains.
Activewear containing high spandex/elastane ratios (15%-30%) undergoes pre-stenter thermal stabilization prior to cutting. Post-sewing steam setting is conducted in tensionless conveyor tunnels under controlled temperatures (typically 160°C to 180°C depending on fiber composition) to prevent elastane breakdown and lock dimensional stability within a +/- 2.5% margin.
Sample development and custom lab dips typically take 7 to 10 working days. Full bulk production and export finishing usually require 25 to 35 days post sample approval, depending on raw material availability and specific washing/finishing complexity.
Request our comprehensive digital product catalog, fabric swatch books, and technical finishing capabilities deck. Connect directly with our engineering team today.