Explore our top-tier OEM/ODM customizable apparel ranges engineered with advanced fabric finishes, seamless knitting, and precise garment-dye capabilities.
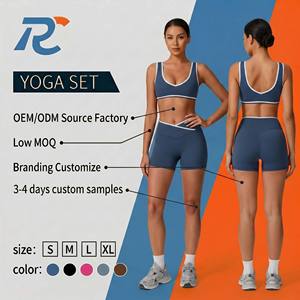
Headquartered in Los Angeles with vertically integrated global manufacturing networks, we bridge high-end Western aesthetic design with industrial scale apparel manufacturing efficiency.
From raw material yarn selection and custom knitting to precision laser-cutting, flatlock stitching, and custom branding appliques, our full-service setup minimizes lead times while maximizing quality control.
Our specialized wash facilities utilize computer-controlled enzyme bath systems, sustainable ozone fading chambers, and mineral pigment dip tanks to achieve consistent vintage fade profiles across mass production runs.
Every batch undergoes rigorous AQL 2.5 inspection, AATCC crocking fastness testing, dimensional shrinkage evaluation, and ISO 105 colorfastness checks to guarantee retail-ready compliance.
Achieving an authentic "sun-faded," vintage aesthetic without compromising fabric tensile strength requires precise chemical formulation and thermal control. Here is how our engineering team guarantees premium results.
In modern fashion procurement, vintage wash apparel is no longer defined merely by surface fading. Today’s luxury streetwear brands and high-end activewear lines require heavy-weight cottons (300 GSM to 500 GSM French Terry and single jersey) that retain structural integrity, seam strength, and soft hand-feel despite aggressive chemical and mechanical distressing.
| Wash Technique | Chemical Agent / Process | Visual Effect & Texture | Fabric Compatibility | Tensile Loss Risk |
|---|---|---|---|---|
| Acid Wash / Snow Wash | Pumice stones soaked in Potassium Permanganate (PP) solution | High-contrast localized marble fading with dark contrast seams | 100% Heavy Cotton Jersey, Denim, Heavyweight Fleece | Medium (Requires Neutralization Bath) |
| Mineral Wash / Pigment Dip | Pigment dye application followed by mild enzyme wash phase | Muted, tonal vintage cast with soft chalky undertones | Cotton Blends, French Terry, Ribbed Fabrics | Low (< 3% Fiber Wear) |
| Ozone Eco-Fade | Gaseous Ozone ($O_3$) oxidation in closed loop tumbler system | Clean, natural sun-bleached look without harsh chemical residue | Organic Cotton, Recycled Polyester Blends | Negligible (< 1% Fiber Wear) |
| Enzyme Stone Wash | Cellulase enzymes combined with synthetic pumice stones | Uniform surface fuzz removal, distressed seam abrasion, ultra-soft feel | Heavyweight Loopback Terry, Fleece Hoodies | Low to Medium |
| Sun-Fade / Reactive Spray | Hand-sprayed reactive dye reduction + UV curing chamber | Gradient shadow vintage fading along shoulders and seams | Streetwear Tees, Oversized Hoodies, Sweatpants | Low |
Traditional piece dyeing colors the fabric roll before cutting. In contrast, Garment Dyeing (GD) stitches PFD (Prepared for Dye) blank garments first, then dyes the completed piece. This enables deep pigment concentration in stitched seams, ribbed necklines, and pockets, yielding the distinct vintage dimensional highlight that modern sourcing directors demand.
Because vintage washes subject raw cotton to hot bath agitation (up to 60°C - 80°C) followed by tumble drying, uncontrolled shrinkage can exceed 8-12%. Full Speed 100 utilizes Pre-Shrunk Pattern Engineering where CAD patterns are oversized by precise lab-tested scale factors, ensuring final post-wash garments land exactly on tech pack measurements.
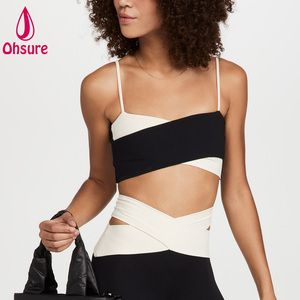
Applying vintage washes to synthetic nylon/spandex or elastane-blended activewear requires modified cationic dyeing procedures. Standard acid wash destroys elastane elasticity. Our specialized low-temperature pigment binder processes allow seamless sports bras, leggings, and workout sets to display retro washed aesthetics while retaining 100% stretch recovery.
Anticipating buyer expectations, regulatory shifts, and technical innovations shaping global apparel procurement over the next decade.
Environmental regulations across the EU and US are tightening around textile wastewater discharge. Sourcing directors are transitioning from traditional stone washing to Nanobubble Ozone and Laser Distressing technologies. These processes reduce water consumption by up to 85% and eliminate heavy chemical baths while producing authentic worn-in textures.
The boundary between performance activewear and luxury streetwear has dissolved. Sourcing metrics show a 140% spike in requests for 380+ GSM vintage washed cotton-poly gym tees, sun-washed oversized hoodies, and distressed seam workout joggers. Buyers require high moisture management alongside authentic vintage aesthetics.
To mitigate inventory risk, modern clothing brands are abandoning massive 5,000-piece single-color commitments. The winning OEM/ODM suppliers are those offering flexible Small Batch Production (100–300 pcs per style/wash) paired with rapid scaling pipelines upon market validation.
A transparent, fully monitored 5-stage manufacturing workflow engineered to guarantee product precision and on-time shipment.
Our CAD engineers review your tech pack, fabric weight target, Pantone/Pantone TPX color references, and wash target samples to formulate the production blueprint.
We formulate custom dye recipes and create 3-option lab dip shade swatches and wash strike-offs for buyer sign-off within 5-7 business days.
A complete PP sample is sewn and processed in our wash lab to evaluate post-wash shrinkage, stitching tension, hand feel, and pattern balance.
Precision automated cutting, high-tensile flatlock sewing, and computer-controlled batch wash tumbler runs are executed under strict quality control.
Final trimming, custom branding tab attachment, individual polybagging, barcode labelling, and expedited global freight delivery to your warehouse.
Detailed technical answers to common queries regarding OEM/ODM vintage wash apparel production, minimums, lead times, and quality assurance.
Partner with an established OEM/ODM apparel manufacturer. Experience rapid sample turnarounds, competitive tier pricing, and uncompromised industrial quality.