Explore our core high-volume apparel manufacturing runs featuring premium combed cotton, DTG digital printing, screen printing, and custom streetwear silhouettes.
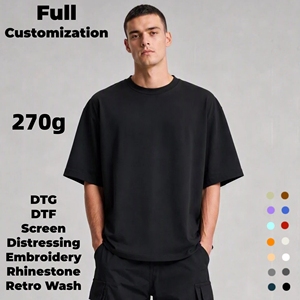
A deep-dive analysis into print application thermodynamics, fabric GSM engineering, and OEM sourcing strategies for international buyers.
The global custom apparel ecosystem has undergone a monumental shift from low-cost basic garment assembly to high-precision, technical OEM/ODM manufacturing. As global fashion brands, corporate distributors, and ecommerce apparel conglomerates demand higher fabric densities, superior wash-fastness, and eco-certified reactive inks, Chinese suppliers have established advanced vertical integration. By consolidating fiber spinning, fabric knitting, Sanforization, automated screen-printing, direct-to-garment (DTG) arrays, and cut-and-sew production under unified quality management systems, China remains the undisputed global epicenter for bulk custom t-shirt exports.
Modern B2B procurement directors no longer search simply for cheap blank t-shirts. The search intent centers on structural fabric integrity, color-fastness ratings above Grade 4, low minimum order quantities (MOQs) for multi-SKU runs, and certified zero-water-pollution ink formulations. This whitepaper breaks down the exact technical parameters and economic factors required to scale bulk t-shirt printing sourcing successfully.
Selecting the optimal printing application directly influences unit cost, hand-feel, durability, and production lead times. Below is a engineering-grade comparison of modern bulk customization technologies utilized across our manufacturing infrastructure:
| Technology | Optimal Order Volume | Fabric Compatibility | Color Gamut & Detail | Wash Durability | Hand-Feel (Touch) |
|---|---|---|---|---|---|
| High-Density Screen Printing | 500 - 500,000+ pcs | 100% Cotton, Blends, Canvas | Pantone Matched (Solid/Halftone) | 50+ Domestic Washes | Medium (Soft Plastisol / Discharge) |
| Industrial DTG (Direct-to-Garment) | 50 - 2,000 pcs | 100% Combed Cotton, High-Cotton Blends | Photorealistic / Unlimited Colors | 35-45 Domestic Washes | Ultra-Soft / Zero-Sensation Ink |
| Direct-to-Film (DTF) Transfer | 100 - 10,000 pcs | All Fabrics (Polyester, Nylon, Cotton) | High DPI Micro-Detail Graphics | 40+ Domestic Washes | Light Rubberized Film |
| Dye Sublimation Printing | 200 - 50,000 pcs | 100% Polyester / Synthetic Technical Mesh | Full All-Over Print (AOP) Vivid | Lifetime (Fibers Permeated) | 100% Seamless / Zero Hand-Feel |
Quality failure in custom printed t-shirts primarily manifests as ink cracking, fading after initial washes, or dye migration (bleeding). To counteract this, our automated production lines utilize German and Japanese eco-friendly inks (OEKO-TEX Standard 100 certified). High-density screen printing employs water-based discharge inks for dark cotton garments, neutralizing the fabric's base dye and bonding deep within the cellulose microfibers rather than sitting as a thick plastic layer on top.
For high-definition graphic streetwear—specifically heavy oversized tees (240 GSM to 300 GSM)—we implement a dual-pass DTG white base pre-treatment protocol. This guarantees that complex CMYK color profiles achieve maximum vibrancy without compromising garment breathability or flexing elasticity.
From raw yarn selection to private-label finishing, examine how our vertical supply chain supports global garment brands.
We source over 100+ fabric formulations: from lightweight 140 GSM combed ring-spun cotton for promotional giveaways to 280-320 GSM French Terry and heavy jersey for luxury streetwear line launches.
Our in-house master pattern makers turn digital sketches, inspirational images, or physical reference samples into production-ready digital tech packs, offering precise grading across XS to 5XL sizing specs.
Every bulk shipment undergoes strict multi-stage quality control. We measure dimensional stability, seam tensile strength, color fastness, weight tolerance (±5g), and print alignment prior to final packing.
We provide comprehensive private label branding services designed to convert stock blank tees into brand-ready merchandise:
Strategic forecast for brand managers, corporate buyers, and apparel supply chain architects.
Consumer preferences have decisively shifted from thin, slim-fit 140 GSM cotton shirts toward boxy, drop-shoulder, heavyweight streetwear constructions (240 GSM to 360 GSM). Sourcing managers must re-align supply chains to accommodate heavier fabric knitting machines, specialized pre-shrunk washing cycles, and heavy-gauge double-needle stitching at neck collar ribs to prevent sagging over time.
ESG compliance is no longer optional in Western markets. Leading buyers mandate GOTS-certified Organic Cotton, Recycled Polyester (rPET), and Bamboo-Cotton Blends. Furthermore, export suppliers in China are increasingly integrating digital product passports (DPP) using QR code labels, allowing end consumers to trace raw cotton origin, knitting factory location, and environmental ink compliance data.
To reduce inventory holding risk, fashion brands are migrating toward agile supply chains. Instead of ordering 50,000 units of a single design once a year, procurement strategies emphasize "Micro-Bulk" initial orders (300 to 1,000 units) backed by rapid 7-day replenishment capabilities. Our automated fabric cutting beds and modular sewing lines are tailored specifically to facilitate this fast-turnaround agile model.
Clear, authoritative answers addressing technical specifications, logistics, and bulk production parameters.
Our standard MOQ for wholesale custom screen-printed or DTG-printed t-shirts is 100 pieces per design/color. For full custom cut-and-sew apparel with custom fabric dyeing or specialized acid washes, the MOQ starts at 300 pieces per colorway.
We utilize high-grade plastisol and water-based inks combined with automated conveyor heat-curing tunnels operating at precise temperatures (160°C to 180°C). Every batch undergoes standardized 40°C machine wash testing (AATCC 61 standard) for 50 continuous cycles.
We accept high-resolution vector files in AI, EPS, PDF, or SVG formats with text outlined. For DTG raster printing, we require 300+ DPI PNG files with transparent backgrounds scaled to true print dimensions.
Physical pre-production samples are completed within 5 to 7 business days. Once sample approval and tech packs are finalized, bulk mass production takes approximately 12 to 18 business days, depending on overall volume and trim complexity.
Yes. We offer precise Pantone Matching System (PMS C / TCX color guide) ink mixing for screen printing and custom fabric dyeing. Color matching tolerances are maintained within a strict Delta E < 1.5 standard.
We offer flexible Incoterms including FOB, CIF, DDP (Delivered Duty Paid), and EXW. Under DDP terms, our logistics partners manage all import tariffs, customs clearance, and final door-to-door delivery directly to your fulfillment warehouse.
Partner with China's premier OEM/ODM custom apparel manufacturer. Speak directly with a senior textile engineer and receive a comprehensive price quote within 24 hours.
Inquire Now