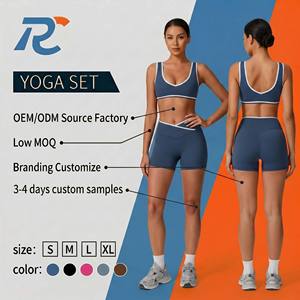
Explore our factory-direct wholesale collections featuring advanced seamless knits, acid-washed finishes, high-impact workout sets, and custom streetwear silhouettes optimized for B2B brand expansion.
In the contemporary apparel manufacturing landscape, the resurgence of 1990s retro aesthetics—specifically acid wash, mineral wash, enzyme distressing, and stone wash finishes—has shifted from a niche subculture trend to a mainstream pillar across activewear, streetwear, and athleisure markets. However, executing consistent, commercial-grade custom acid wash clothing at scale requires complex chemical mastery, precise fabric formulation, and strict environmental compliance.
Selecting a premier China custom acid wash clothing factory is no longer simply about finding low-cost cut-and-sew labor. Global apparel buyers, private label brands, and enterprise sourcing directors demand specialized washing technology, zero-color-bleeding guarantees, high fabric tensile strength retention, and flexible Minimum Order Quantities (MOQs). This comprehensive guide analyzes the operational physics of modern garment washing, material sourcing parameters, eco-friendly technological shifts, and strategic supplier selection frameworks.
True acid washing originally involved soaking porous volcanic pumice stones in oxidizing solutions—traditionally potassium permanganate ($KMnO_4$)—and tumbling them with dry garments to strip surface dyes selectively, creating high-contrast marbled textures. Modern production in top-tier Chinese facilities has evolved significantly toward sustainable, bio-engineered alternatives.
The classic high-contrast wash technique. Volcanic stones are saturated with $KMnO_4$ and tumbled dry with cotton or blended heavy fleece. Yields sharp, aggressive contrast highlights. Requires neutralize baths with sodium metabisulfite to freeze color oxidation.
Next-generation sustainable washing. Laser machinery burns high-resolution vintage patterns onto synthetic or cotton textiles, followed by atmospheric ozone gas processing. Eliminates toxic chemical runoff and reduces water utilization by up to 70%.
Utilizes cellulase enzymes to break down micro-fibrils on the yarn surface, creating a buttery soft hand-feel combined with subtle, weathered color fading. Prevents pilling while imparting an authentic vintage patina without damaging spandex structural integrity.
To assist apparel buyers in drafting precise Tech Packs, the following matrix compares the chemical, structural, and commercial parameters of mainstream washing treatments deployed by Chinese manufacturers.
| Wash Category | Ideal Fabric Composition | Colorfastness (ISO 105-C06) | Tensile Strength Loss | MOQ Threshold | Eco-Impact Level |
|---|---|---|---|---|---|
| Classic Acid Wash | 100% Cotton / 320+ GSM French Terry | Grade 3.5 - 4.0 | 8% - 12% | 300 Pcs / Color | Moderate to High |
| Mineral Dye & Wash | 95% Cotton / 5% Elastane Blends | Grade 4.0 | 5% - 8% | 200 Pcs / Color | Moderate |
| Bio-Enzyme Soft Wash | Nylon/Spandex & Polyester Athletic Blends | Grade 4.5 | < 3% | 100 Pcs / Color | Low (Eco-Friendly) |
| Ozone Laser Distressing | Cotton-Poly Activewear & Seamless Fabrics | Grade 4.5+ | < 2% | 100 Pcs / Color | Ultra-Low (Zero Liquid Discharge) |
The intersection of functional sportswear and vintage streetwear is driving rapid technological innovation in fabric engineering and wash chemistry. Brand directors looking to maintain a competitive edge must align with Chinese production partners who are actively pioneering the following forward-looking manufacturing paradigms:
Traditionally, acid washing was restricted to 100% heavy woven cottons or loopback jersey due to chemical degradation risks on elastane. Modern Chinese knitting facilities have engineered heat-stabilized synthetic yarn blends (such as micro-nylon mixed with acid-wash-receptive cotton-poly face yarns). This enables seamless 3D-knit leggings, ribbed crop tops, and body-sculpting sports bras to undergo rich marble washing without losing recovery torque or shape retention.
Driven by stringent EU Green Deal standards and North American brand sustainability mandates, leading Chinese dye houses are replacing heavy metal oxidizing agents with biodegradable organic peroxide agents and closed-loop ozone wash barrels. This tech achieves the identical high-contrast aesthetic while meeting OEKO-TEX Standard 100 Class I and ZDHC (Zero Discharge of Hazardous Chemicals) Level 3 compliance.
Sourcing demand is shifting away from ultra-lightweight fast fashion toward high-GSM structure. European and US markets are prioritizing 380-500 GSM combed cotton hoodies, 260 GSM boxy drop-shoulder tees, and double-layered ribbed tank tops. China's fabric supply chain provides custom garment-dyeing base colors designed specifically to bleed predictably during acid treatment, yielding deep multi-dimensional shadow seams.
Mass customization is accelerating. Instead of uniform batch washing, advanced facilities combine computerized laser surface ablation with micro-spray wash effects. This allows brands to request variable levels of distressing—such as targeted shoulder fade, vintage graphic cracking, and distressed hem edges—configured dynamically via digital Tech Pack files.
Partnering with an established apparel manufacturing ecosystem ensures complete operational visibility across every phase of garment construction. Building premium custom activewear and acid wash apparel requires seamless integration between raw material sourcing, precision cut-and-sew master craftsmanship, specialized wet processing, and final branding applications.
Our in-house pattern masters utilize computerized CAD marker systems to convert line drawings or physical reference samples into production-ready digital grading specs across XS to 5XL sizing, accounting precisely for post-wash fabric shrinkage.
Direct access to over 100+ audited textile mills offering GOTS-certified organic cotton, recycled polyester, buttery-soft nylon elastane, heavy French terry fleece, and custom knitted ribbing in custom Pantone dye colors.
State-of-the-art sewing lines equipped with 4-needle 6-thread flatlock machines, automated pocket setters, bar-tack reinforcement machinery, and high-tensile elastic coverstitching tailored specifically for performance gear.
Comprehensive branding application suite: high-density 3D puff embroidery, discharge screen printing, puff print, reflective heat transfer vinyl, custom neck labels, woven side tags, and eco-friendly hangtags.
Designed to support emerging luxury labels and scaling activewear brands. Prototype samples are executed in 3 to 5 business days, with flexible initial production batches starting at low minimum thresholds.
Every batch undergoes 100% inline inspection during sewing, followed by post-wash dimensional stability tests, seam-strength pull tests, colorfastness checks, and final packaging according to strict AQL 2.5 standards.
Key technical and logistical questions answered by senior garment engineers to streamline your sourcing workflow.
Connect directly with our engineering team to review Tech Packs, request fabric swatches, or receive a fast enterprise wholesale quote within 24 hours.