Explore our high-performance ODM/OEM production lines, engineered with 4-way stretch compression, moisture-wicking micro-polyester blends, and ergonomic flatlock stitching for global retail export.
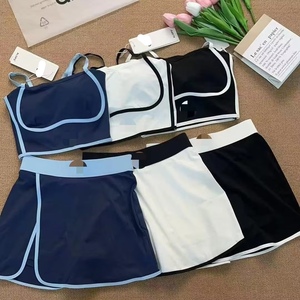
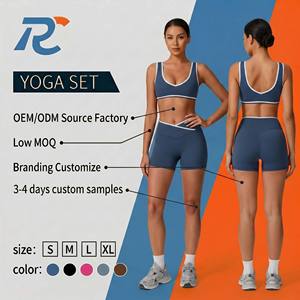
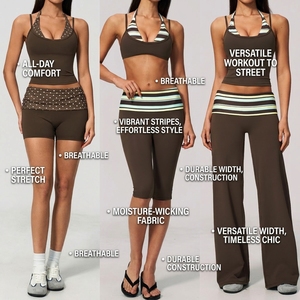
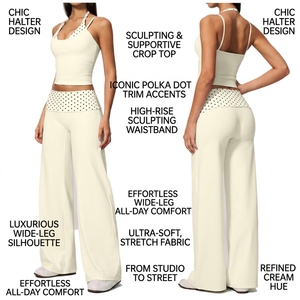
In modern global apparel procurement, shifting from basic Cut-Make-Trim (CMT) contracting to Full Package Production (FPP) represents a critical strategic advantage for retail brands, athletic wear lines, and private label importers. A true Full Package Clothing Manufacturer manages every single tier of the garment supply chain: from raw yarn procurement, fabric knitting, laboratory color matching (Lab Dips), and 3D digital pattern sampling to final precision cutting, custom branding application, quality inspection, and international freight logistics.
| Production Model | Sourcing Responsibility | Tech Pack & Grading | Quality Control (AQL) | Best Suited For |
|---|---|---|---|---|
| CMT (Cut-Make-Trim) | Buyer supplies all fabric & trims | Buyer provides pre-graded patterns | Factory only verifies assembly stitches | Established brands with local fabric mills |
| OEM (Original Equipment Mfg) | Factory sources based on exact specs | Factory follows customer Tech Pack | AQL 2.5 standard inline inspection | Scaling brands seeking cost efficiency |
| FPP / ODM (Full Package) | Full turnkey: Fabric development to packaging | Complete in-house pattern & 3D sampling | End-to-end laboratory & garment testing | Growth brands & high-volume retail exporters |
By unifying Los Angeles design standard sensibilities with China’s unmatched textile manufacturing scale, our vertical integration solves the historic friction points of apparel manufacturing: quality volatility, delayed lead times, and opaque supply networks.
Our master pattern makers translate rough sketches, 2D vector flat renders, or physical benchmark garments into CAD tech packs. Utilizing 3D CLO software, we execute digital fit adjustments to eliminate expensive physical sample revisions, ensuring precise neck drop, chest width, and seam tension tolerances.
Access over 100+ audited material mills specializing in GOTS organic cottons, OEKO-TEX Standard 100 certified synthetics, recycled Repreve® nylon, and antimicrobial activewear textiles. We custom-dye pantone colors with colorfastness ratings exceeding Grade 4.5.
From high-density 3D puff embroidery and silicone gel printing to reflective heat transfer vinyl (HTV) and sublimation printing. Every logo application undergoes rigorous 50-cycle wash tests to prevent peeling, cracking, or color bleeding.
Every production run executed across our facilities follows strict ISO 9001 and AQL 2.5 Major / 4.0 Minor inspection guidelines. We ensure that what you approve during the sample stage is exactly what lands on your warehouse floor.
The global apparel sourcing environment is rapidly shifting under the dual pressures of environmental legislation, supply chain volatility, and consumer demand for instant product turnarounds. Exporters and brand procurement heads must adapt to several macro trends defining the next decade:
Global brands are mandating traceable, low-carbon synthetic materials. Future procurement priorities emphasize bio-based nylon derived from castor oil, recycled ocean plastics, and closed-loop water treatment system dyes. Exporters with OEKO-TEX and GRS (Global Recycled Standard) certifications will dominate preferred supplier matrices.
Traditional sample development cycle times (typically 4–6 weeks) are being compressed into 48-hour digital workflows. Utilizing 3D avatar drape rendering, fashion labels approve fabric fall, strain maps, and print placement digitally, cutting physical prototyping waste by up to 75%.
With upcoming Digital Product Passport (DPP) regulations in Europe and North America, clothing factories must provide complete chain-of-custody data—tracing raw cotton harvests or synthetic polymerization down to the specific spinning mill and cut & sew facility.
The convergence of athletic performance gear and everyday casual fashion ("Athleisure") has elevated consumer expectations regarding garment comfort, durability, and aesthetic features. Key product engineering developments include:
Modern activewear demands multi-dimensional performance attributes built directly into the yarn matrix rather than superficial topical sprays:
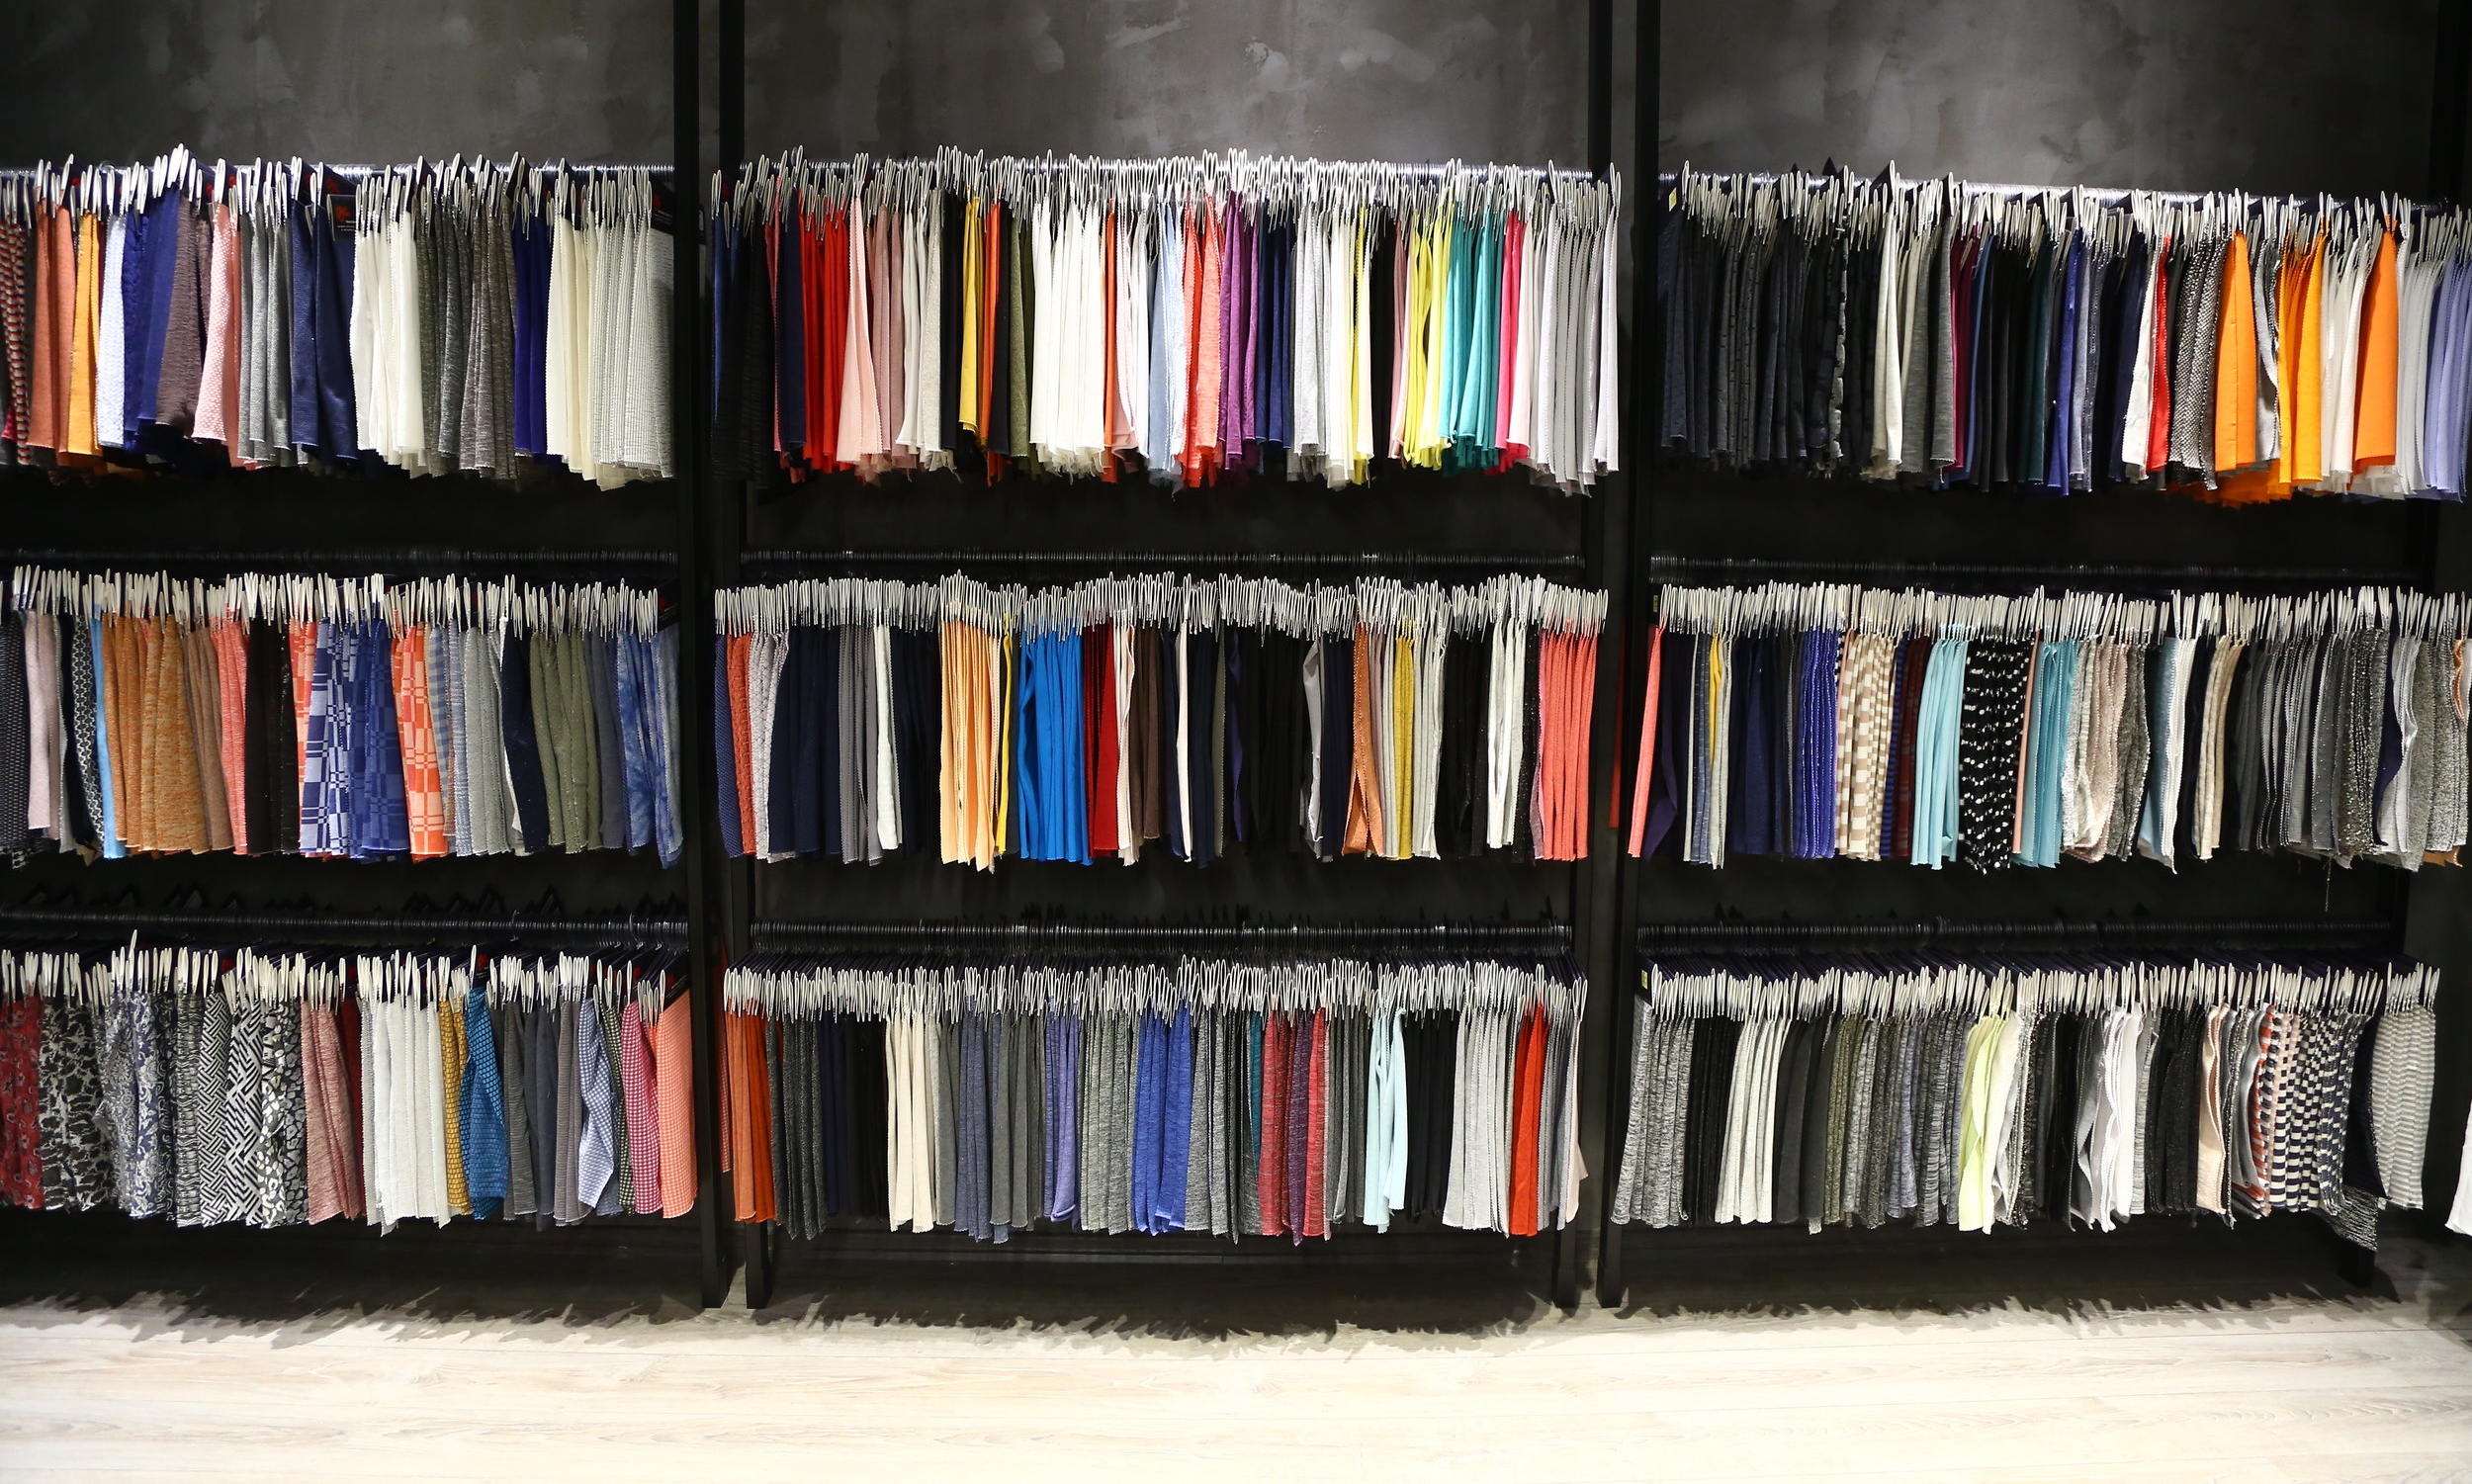
Whether launching a capsule collection or re-platforming an existing garment line, our production facilities supply comprehensive private label finishing options tailored to international distribution standards.
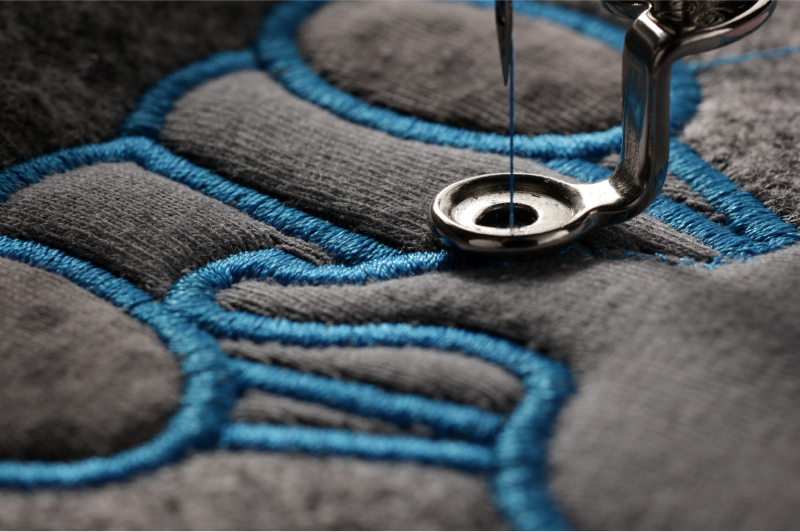
Tajima high-speed computerized embroidery heads delivering flat, 3D puff, applique, and metallic thread embroidery with automated backing trimmers.
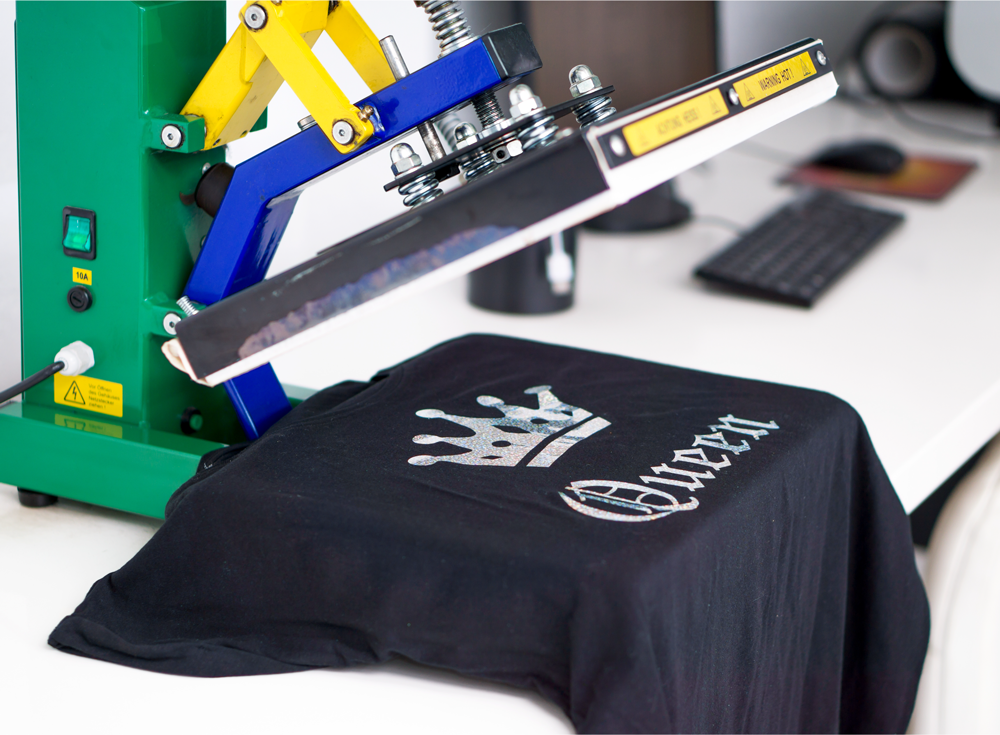
Tagless neck size prints, matte silicone transfer badges, holographic foil designs, and high-visibility reflective transfers for athletic safety.
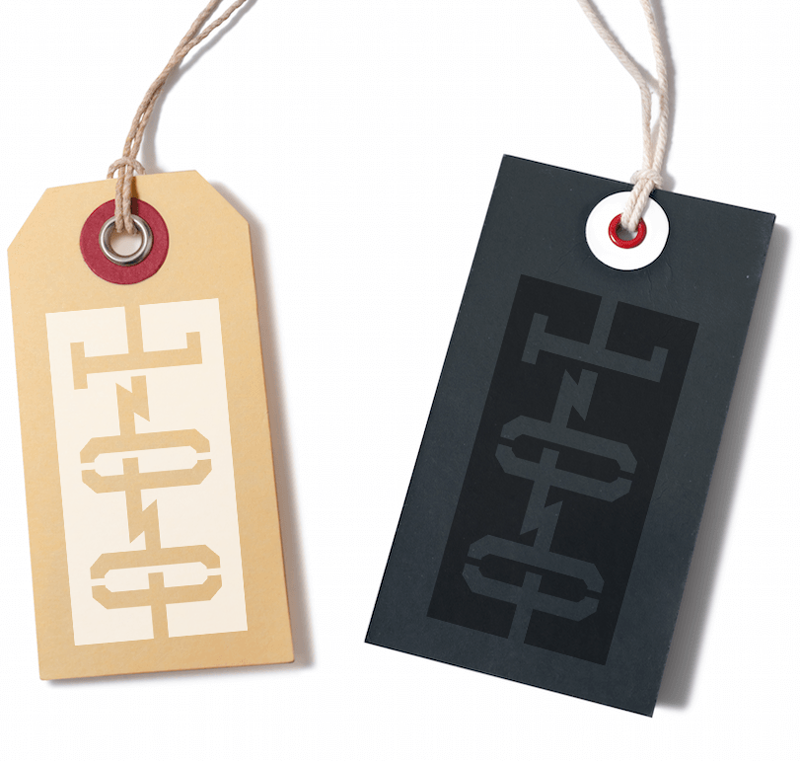
Woven damask main labels, eco-friendly FSC certified paper hang tags, custom polybags with warning prints, and branded zip closures.
Essential technical and operational insights for global procurement managers, brand founders, and apparel buyers sourcing from China full package garment factories.