Explore our high-performance technical activewear portfolio engineered with high-definition digital dye-sublimation, moisture-wicking micro-polyester blends, and precision cut-and-sew architecture for high-end sportswear brands.
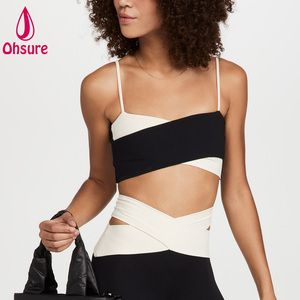
In the hyper-competitive global activewear market, selecting top-trusted sublimation sportswear production manufacturers is no longer merely an operational decision—it is a strategic pillar for brand longevity. Sublimation printing has revolutionized technical athletic apparel by permanently bonding eco-friendly disperse dyes into synthetic textile microfibers under extreme thermal conditions (200°C / 400°F). Unlike traditional surface printing methods such as screen printing or direct-to-garment (DTG), dye-sublimation preserves 100% of the fabric's natural moisture-wicking pore network while delivering infinite color complexity, Zero-Feel tactile weight, and absolute peel-proof durability.
Full Speed 100 operates as an end-to-end clothing manufacturer headquartered in Los Angeles, CA. By controlling every stage of the apparel creation pipeline—from preliminary tech pack engineering to pattern grading, fabric sublimation, cut & sew production, and final quality control—we eliminate middleman friction and guarantee factory-direct pricing for private label brands.
Our Los Angeles pattern-making team converts artistic sketches and mood boards into production-ready vector tech packs, 3D CAD patterns, and multi-size grading rules to ensure perfect ergonomic compression fits across all size curves.
We source specialized performance textiles directly from domestic and international mills: recycled PET polyester, elastane blends, anti-microbial nylon, four-way stretch interlocks, and lightweight mesh optimized for thermal sublimation ink absorption.
Utilizing non-toxic, eco-certified Italian digital dye inks, our high-pressure calendar rollers deliver photorealistic color vibrancy, razor-sharp geometric precision, and total resistance to UV fading or salt-water breakdown.
Once fabrics are sublimated, our master seamstresses employ specialized flatlock flat-seam machines, 4-needle 6-thread stitching, and reinforced bar-tacking to eliminate skin friction and handle high-strain athletic activity.
We empower emerging athletic labels, sports academies, fitness influencers, and corporate enterprises by offering flexible low Minimum Order Quantities (MOQs), enabling rapid design testing without heavy capital expenditure.
Every garment batch undergoes rigorous physical inspection: stitch elasticity tension tests, color fastness wash evaluations, seam burst strength analysis, and dimensional stability checks prior to custom re-labeling and dispatch.
Understanding the physical and chemical differences between fabric decoration methodologies is crucial when building a premium activewear product line. Review how digital dye-sublimation outperforms legacy screen printing and DTG processes.
| Performance Metrics | Dye-Sublimation Printing | Traditional Screen Printing | Direct-To-Garment (DTG) |
|---|---|---|---|
| Color Molecule Integration | Gas-Phase Fiber Bonding | Surface Ink Layer Deposit | Surface Micro-Droplet Binding |
| Breathability & Wicking | 100% Pore Preservation | Blocked Fabric Air Pores | Partial Airflow Restriction |
| Peeling, Cracking & Fading | Zero Risk (Permanent) | High Risk After 25+ Washes | Moderate Risk Over Time |
| Design Complexity & Colors | Unlimited Gradient / Photorealistic | Limited (Charged Per Screen) | High (CMYK Dependent) |
| Hand-Feel (Tactile Weight) | Zero-Feel (Weightless) | Heavy Rubberized Feel | Soft to Medium Texture |
| Ideal Fabric Composition | 100% Polyester / Poly-Elastane Blends | 100% Cotton / Heavy Blends | High Cotton Content Fabrics |
Modern high-intensity activewear requires engineered fabrics capable of handling intense mechanical stretch while managing body thermoregulation. When sublimating polyester-elastane substrates (such as 82% Recycled Polyester / 18% Spandex), exact heat transfer calibration at 195°C to 205°C prevents elastomer thermal degradation, preserving full dynamic recovery and dynamic muscle compression during extreme physical training.
As consumer demands shift toward sustainable activewear, instant customization, and intelligent moisture control, B2B sportswear procurement managers must adapt to modern supply chain shifts.
Sustainability is now a core requirement. Global brands are shifting toward post-consumer recycled polyethylene terephthalate (rPET) yarns derived from ocean-bound plastics. Combined with waterless disperse dye printing, this dramatically reduces carbon footprints while maintaining high print brilliance.
Next-generation sublimation sportswear integrates silver-ion antimicrobial coatings and capillary-action channel knitting. Fabrics wick sweat away from skin micro-pores to the outer garment surface, enabling rapid evaporation during high-endurance workouts.
To mitigate international shipping delays and inventory markdowns, brand owners are partnering with full-service USA-based hubs like Full Speed 100 in Los Angeles. Localized cut & sew sample validation speeds up market launches from months to days.
Expert technical answers to common questions regarding minimum order quantities, vector artwork, fabric selection, and full-scale OEM sportswear manufacturing.
Partner with Full Speed 100 for end-to-end cut & sew apparel development, premium material sourcing, and high-definition dye sublimation in Los Angeles.