Explore our primary export apparel series engineered with superior colorfastness, non-bleed reactive dyeing, and precision Pantone lab-dip matching compliant with EU REACH standards.
Norway’s apparel, outdoor, and technical textile sectors operate under some of the most rigorous environmental and safety mandates globally. As European Union standards tighten under the EU Strategy for Sustainable and Circular Textiles, Norwegian brands, industrial importers, and commercial apparel lines require fabric dyeing partners that unite hyper-accurate color matching with absolute regulatory verification.
While CE marking traditionally applies to personal protective equipment (PPE) and functional protective garments under EU Regulation 2016/425, Norwegian commercial buyers and custom clothing brands increasingly demand CE-level traceability and test reports across all dyed fabric components. Our dyeing mills implement comprehensive quality control frameworks aligned with European standardisation protocols.
Strict prohibition of carcinogenic Azo dyes, SVHCs (Substances of Very High Concern), heavy metals (lead, cadmium, nickel), and alkylphenol ethoxylates (APEOs/NPEOs). Our chemical dye baths are certified 100% compliant for Norwegian customs clearance.
Guaranteed skin-safe chemical residue limits. Tested specifically for infant-grade direct skin contact, ensuring zero skin irritation, formaldehyde traces, or volatile organic compound (VOC) emissions during wearing and washing.
Formulated to satisfy Scandinavian eco-procurement tenders. Incorporating reduced water-to-cloth liquor ratios (1:4 to 1:6), bio-degradable levelling agents, and strict effluent chemical oxygen demand (COD) monitoring.
Achieving long-lasting color intensity without compromising fabric hand-feel, breathability, or tensile strength demands specialized dye chemistry tailored to specific fiber polymer structures.
Target Substrates: Organic Cotton, Viscose, Bamboo, Modal.
Forming covalent bonds directly with cellulose molecules, reactive dyestuffs yield brilliant color brilliance and outstanding fastness to repeated industrial laundering up to 60°C. Ideal for high-end Norwegian lifestyle apparel and everyday wear.
Target Substrates: Polyester (rPET), Polyethylene, Synthetic Blends.
Utilizing high-temperature carrier-free pressure vessels at 130°C–135°C, disperse dye molecules migrate deep into hydrophobic synthetic microfibers, eliminating color fading caused by intense friction and active stretch stress.
Target Substrates: Norwegian Merino Wool, Silk, Polyamide (Nylon 6 / 6.6).
Specifically formulated to protect natural wool fiber scales while delivering rich shade depth. Ensures superior resistance to perspiration, ozone, and salt-water exposure, critical for Scandinavian winter activewear.
Norway’s unique geography, arctic weather patterns, and maritime economy demand fabric coloration solutions engineered for extreme operational environments.
Norwegian ski brands and expedition outfitters require high UV lightfastness (ISO 105-B02 Grade 6+) to combat sunlight reflectance off snow fields. Our solution-dyed synthetic yarns and thermo-stabilized acid-dyed wool preserve color saturation even under prolonged sub-zero, high-altitude UV radiation.
Vessels operating in the North Sea and coastal fish-farming infrastructure expose workwear to continuous saltwater spray and alkaline oils. Our heavy-duty vat and cationic dyeing methods prevent color bleeding, salt-crystallization degradation, and sea-water crocking (ISO 105-E02 fastness grade 5).
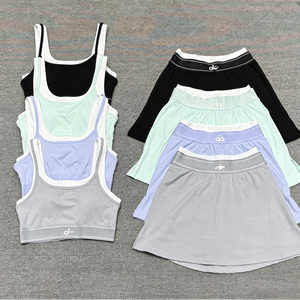
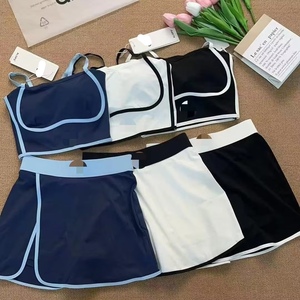
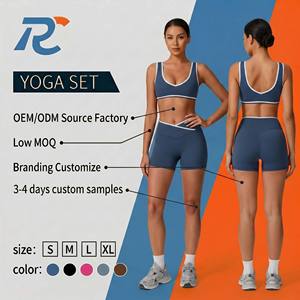
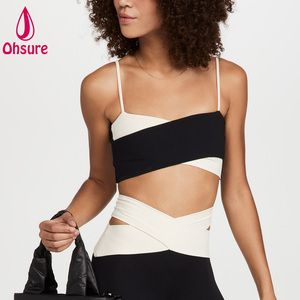
For Norwegian boutique activewear labels (such as two-piece workout sets, sports bras, and seamless leggings), color migration during intense cross-stretching can cause ugly white-out lines. Our high-penetration micro-emulsion dye baths guarantee 100% core fiber coverage across 4-way stretch fabrics.
Modern fitness garments combine high-contrast panels (e.g., stark white trims against deep navy blue or black body panels). Standard dyeing often results in thermo-migration or color bleeding during heat-pressing logos or high-temp wash cycles. Full Speed 100 utilizes specialized anti-migration fixing agents and high-fastness disperse dyes that undergo rigorous 180°C hot-pressing migration testing, guaranteeing clean contrast lines and crisp panel separation.
Understanding local consumer preferences and supply chain mandates in Oslo, Bergen, Trondheim, and Stavanger.
Norwegian brands lead the shift toward post-consumer recycled fabrics (rPET, Econyl® regenerated nylon, post-consumer recycled wool). Dyeing recycled polymers requires precise temperature control and specialized leveling auxiliaries to achieve uniform shade batch-to-batch, despite variations in recycled feedstock color.
With Scandinavian consumers prioritizing sustainability, brands highlighting reduced water footprints gain strong market share. Our facilities incorporate Cold Pad-Batch (CPB) dyeing and modern air-flow dye jet machinery that cuts water consumption by up to 60% compared to traditional winch dyeing.
Nordic design aesthetics favor muted, sophisticated earth tones (slate gray, fjord green, arctic white, deep ochre, sand). Matching subtle neutral shades requires advanced Datacolor spectrophotometer formulation to eliminate metamerism (color shifting under store fluorescent vs. natural Nordic daylight).
By combining custom fabric dye kettles with our end-to-end garment production infrastructure, we remove intermediate broker markups, eliminate quality hand-off errors, and accelerate delivery times for Norwegian apparel brands.
Send us your digital Pantone TPX/TCX codes or physical fabric swatches. Our spectrophotometer-guided laboratory delivers 3-option lab dip shade trees (A, B, C options under D65, TL84, and A lighting) within 3 to 5 business days.
Unlike traditional industrial dye houses requiring 1,000+ kg per shade, our sample-dye kettles and flexible jet vessels accommodate low minimum order quantities (from 50 kg for custom fabric, or 100 sets for custom-dyed finished garments).
From raw yarn sourcing, custom knitting/weaving, vat dyeing, and finishing (water-repellent, anti-microbial, anti-pilling) to precision cutting, sewing, and custom branding applications (embroidery, screen print, heat transfer).
Essential answers covering international customs paperwork, test certifications, environmental standards, and production logistics.
Every shipment exported to Norway includes a complete Technical Compliance Package. This contains REACH Annex XVII chemical testing declaration reports, OEKO-TEX® Standard 100 Class I certificates, Azo-dye free verification, and independent lab test results for colorfastness to washing (ISO 105-C06) and rubbing (ISO 105-X12). For protective workwear, relevant EN ISO test certificates are attached.
We utilize Datacolor 800 Spectrophotometric computerized color recipe archives. Each approved lab dip generates a digital spectral reflectance curve. When re-ordering, the automated dye dispensers reconstitute the exact chemical dye formulation, maintaining a color difference tolerance of Delta E (ΔE) < 0.3 against the master standard.
Yes. We specialize in color formulations for 100% GRS (Global Recycled Standard) certified post-consumer recycled polyester and recycled polyamide 6.6. Our low-impact disperse dye processes ensure deep shade saturation without degrading the tensile strength or elasticity of recycled microfibers.
Lab dip shade matching requires 3 to 5 business days. Once approved, bulk fabric dyeing typically takes 10 to 14 days depending on total meterage. Air express delivery to major Norwegian airports (Oslo Gardermoen, Bergen Flesland) takes 3 to 5 days, while ocean freight to Norwegian ports takes approximately 22 to 28 days.
We provide full DDP (Delivered Duty Paid) or DAP (Delivered at Place) terms. All commercial invoices, HS commodity code classifications, country-of-origin certificates, and REACH compliance declarations are pre-filed to ensure smooth processing through Norwegian Customs (Tolletaten) without unexpected delays.
Simply click the live chat quote button on this page. Share your target fiber composition, color Pantone codes, required fabric weight (GSM), total meterage, and any specific finishing requirements (e.g., moisture wicking, flame retardancy, UV resistance). Our textile engineering team will provide a comprehensive quotation within 24 hours.
Partner with a certified industrial manufacturer that delivers precise color matching, zero-compromise EU regulatory compliance, and rapid turnaround for Scandinavian markets.